中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
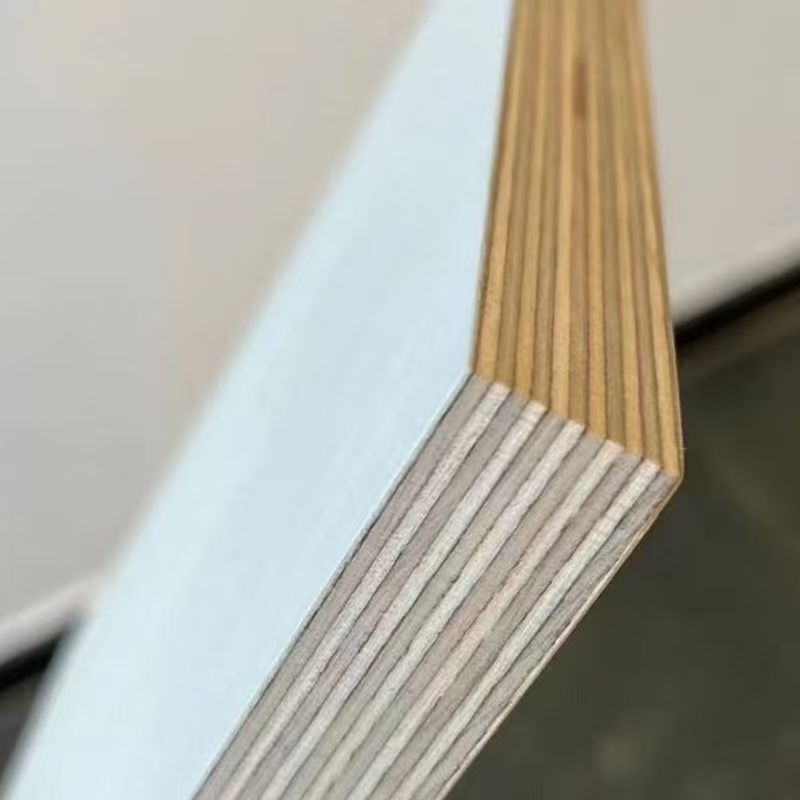
I. Basic Concept of Plywood
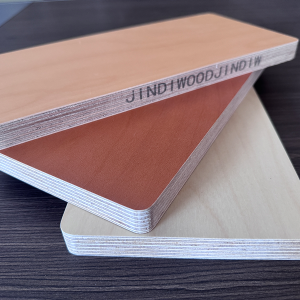
Plywood is a panel material with three or more odd-numbered layers, manufactured by rotary-peeling logs into veneers or slicing timber into thin sheets, assembling them with the grain direction of adjacent layers perpendicular to each other, bonding with adhesives, and hot-pressing.
This "odd-numbered layers, adjacent perpendicular" structural design is the core logic of plywood technology: it effectively eliminates deformation defects caused by wood anisotropy (longitudinal strength far exceeds transverse strength), giving plywood nearly uniform physical and mechanical properties in both longitudinal and transverse directions. Its bending strength, impact resistance, and dimensional stability are significantly superior to natural solid wood of the same thickness.
Key Data: High-quality plywood can achieve longitudinal MOR of 60-100 MPa and MOE of 6000-10000 MPa, far exceeding ordinary solid wood.
II. Plywood Manufacturing Process Flow
2.1 Raw Material Preparation
Log Selection: Plywood requires relatively high-quality logs. Common species include:
| Species | Characteristics | Main Applications |
|---|---|---|
| Poplar | Light, soft, good rotary peeling properties, economical | Core layers of mid-to-low grade plywood |
| Pine | Straight grain, high strength, good corrosion resistance | Construction formwork, packaging boards |
| Eucalyptus | Fast-growing, moderate density, smooth peeling surface | Furniture panels, flooring substrates |
| Birch | Dense texture, high strength, light color | High-end furniture, aircraft plywood |
| Meranti | Strong weather resistance, excellent bonding properties | Marine plywood, exterior-grade panels |
| Okoume | Uniform texture, excellent peeling properties | Decorative veneer panels, speaker boards |
Log Processing:
Cross-cutting: Logs are cut to predetermined lengths (typically 2600-2800mm) to suit the maximum processing size of the peeling lathe.
Steaming/Water Heat Treatment: Logs are placed in steaming pits at 60-90°C for 24-72 hours (depending on species and season). This treatment increases wood plasticity, homogenizes moisture content, ensures continuous and smooth veneer peeling, and softens resin to reduce cutting resistance.
Debarking: A debarker removes bark to prevent bark impurities from contaminating the veneer and to protect the peeling knife.
2.2 Veneer Peeling
This is the core process of plywood production. The log rotates at high speed on the peeling lathe, while a sharp peeling knife feeds radially and parallel to the log, continuously and uniformly cutting the log into an endless veneer strip — similar to the principle of a pencil sharpener, but in reverse.
Veneer Thickness: Typically 0.6-4.2mm; common specifications: 1.0mm, 1.5mm, 2.0mm, 2.5mm
Peeling Precision Control: Thickness tolerance must be controlled within ±0.05mm
Veneer Yield: Rotary peeling achieves a veneer yield of 75-85%, far higher than sawing (approx. 40-50%)
The peeled veneer is in a continuous strip form and is cut into sheets by a guillotine shear according to required dimensions, or wound into rolls for storage.
2.3 Veneer Drying
Freshly peeled veneer has extremely high moisture content (60-120%) and must be dried immediately to prevent mold and discoloration. Another core purpose of drying is to control moisture content within the requirements of the gluing process, preventing blistering and delamination caused by moisture vaporization during hot pressing.
Drying Equipment: Mesh-belt veneer dryers (roller dryers), jet veneer dryers
Drying Temperature: Typically 160-200°C (high temperature for rapid evaporation at inlet; temperature reduced at outlet for moisture equalization)
Target Moisture Content After Drying: 8-12% (national standard for finished plywood: 6-14%)
Drying Quality Control: Excessive moisture content → blistering during hot pressing; too low moisture content → brittle veneer, poor glue absorption
Dried veneers are sorted by grade (face/back veneers, core veneers, repair veneers, etc.), and defects such as knots and cracks are repaired (using patch embedders) to ensure face veneers are defect-free.
2.4 Glue Application and Lay-up
Glue Application: Adhesive is uniformly applied to the veneer surface. Precise glue application control is essential — insufficient glue leads to inadequate bonding strength; excessive glue increases costs and may cause glue bleed-through contaminating the surface.
Application Method: Roller coating (double-roller or four-roller glue spreaders); veneer passes through the gap between upper and lower glue rollers, with a uniform adhesive layer deposited on the surface.
Glue Spread Rate: Typically 180-220 g/m² (both sides combined); the industry standard unit is "wet glue weight."
Adhesive Types: See Section III for details.
Lay-up: Following the principle of "adjacent veneer layers with perpendicular grain directions," the glued veneers are stacked together to form a mat.
Odd-Numbered Layers: 3, 5, 7, 9 layers, etc. (Symmetry principle: veneer thickness, species, and moisture content on both sides of the center layer should be consistent to prevent warping.)
Face and Back Veneers: High-quality veneers (defect-free, attractive grain)
Core Veneers: Lower-grade veneers, with small splices allowed (longitudinal extension, lateral widening)
2.5 Pre-Pressing and Hot Pressing
Pre-Pressing (Cold Pressing): The mat is pressed at room temperature under relatively low pressure (typically 0.8-1.2 MPa) to allow the adhesive to initially wet the veneer surfaces and set the mat, preventing it from falling apart before entering the hot press. Pre-pressing time: typically 10-30 minutes.
Hot Pressing: This is the most critical process in plywood production, directly affecting the product's bonding strength, moisture content, flatness, and formaldehyde emission.
| Hot Pressing Parameter | Typical Range | Effect |
|---|---|---|
| Temperature | 120-160°C (PF: 140-160°C; UF: 120-140°C) | Too high → wood thermal degradation, adhesive aging; too low → insufficient adhesive curing |
| Pressure | 1.0-2.5 MPa (depending on board thickness and species) | Too high → veneer crushing, excessive density; too low → poor bonding |
| Time | 0.6-1.2 min/mm board thickness (e.g., 18mm board: 10-20 min) | Too short → incomplete adhesive curing; too long → reduced production efficiency, excessive wood carbonization |
Core Principle of Hot Pressing: High temperature causes the adhesive to undergo cross-linking curing reactions, firmly bonding adjacent veneers; simultaneously, pressure densifies the mat, eliminating inter-layer voids.
2.6 Trimming and Sanding
Trimming: The rough-edged boards from hot pressing are trimmed to standard dimensions (e.g., 1220×2440mm) on a trimming saw, removing glue nodules and edge defects.
Sanding: Board surfaces are sanded on wide-belt sanders to achieve precise thickness and a smooth, flat surface, providing a good foundation for subsequent finishing.
Sanding Grit Sequence: 60 grit → 120 grit → 180 grit (rough to fine, staged sanding)
Thickness Tolerance Control: Finished product thickness deviation controlled within ±0.3mm
2.7 Grading and Packaging
Finished boards are sorted by appearance grade and physical performance grade, labeled, bundled, and warehoused.
Appearance Grades: National standard GB/T 9846 divides plywood appearance into Premium, First Class, and Qualified grades.
Packaging Standards: Export products are packaged with moisture-proof paper + plastic film + edge protectors + steel/plastic strapping.
III. Adhesive Technology: Determining Plywood Performance and Environmental Grade
Adhesives are the "lifeblood" of plywood, directly determining the product's bonding strength, water resistance, and environmental grade. Different adhesive types suit different applications:
| Adhesive Type | Water Resistance | Applications | Environmental Grade | Curing Temperature |
|---|---|---|---|---|
| Urea-Formaldehyde (UF) | Dry conditions | Indoor furniture (low-end) | E1/E0 | 120-140°C |
| Melamine-Modified UF (MUF) | Moderate | Indoor furniture (mid-to-high-end) | E0/ENF | 130-150°C |
| Phenolic Resin (PF/WBP) | Boil-proof | Marine plywood, formwork | E0 | 140-160°C |
| Isocyanate (MDI) | Excellent | Formaldehyde-free boards, OSB | ENF/HENF | 100-130°C |
| Soy Protein Adhesive | Moderate | Eco-friendly furniture boards | ENF | Approx. 120°C |
WBP (Water Boil Proof) is a bonding strength grade specified in the BS 1088 marine plywood standard, meaning "boil-proof grade" — the adhesive layer remains intact after 72 hours of boiling. Plywood achieving WBP grade can be used outdoors and in humid environments for extended periods.
Bonding Strength Technical Specifications (GB/T 9846):
| Item | Premium | First Class | Qualified |
|---|---|---|---|
| Average Bonding Strength (MPa) | ≥0.70 | ≥0.70 | ≥0.70 |
| Minimum Veneer Bonding Strength (MPa) | ≥0.60 | ≥0.60 | ≥0.50 |
| Specimen Pass Rate | ≥95% | ≥90% | ≥85% |
Note: BS 1088 marine plywood standard requires bonding strength ≥1.0 MPa, higher than the national standard.
IV. Core Technical Specifications and Test Methods
4.1 Bonding Strength
Bonding strength is the core indicator measuring the inter-layer adhesion of plywood, directly determining whether the board will delaminate during use. The test method is tensile shear testing:
Standard specimens are cut from the board, with grooves cut at both ends to expose the adhesive layer
A universal testing machine applies tensile load along the adhesive layer direction
The maximum load at failure is recorded and divided by the bonding area to obtain bonding strength (MPa)
Failure Mode Assessment: Qualified products should exhibit wood failure ≥80% (i.e., the adhesive layer does not fail; the wood itself fractures first), indicating that bonding strength exceeds the wood's own strength.
4.2 Moisture Content
Moisture content affects the board's dimensional stability, workability, and risk of deformation during subsequent use.
Test Method: Gravimetric method (dried to constant weight at 105±2°C)
National Standard: Plywood moisture content is 6-14%, adjustable by agreement based on regional service environments.
4.3 Modulus of Rupture and Modulus of Elasticity
These are core mechanical indicators measuring the board's load-bearing capacity, especially important for construction formwork and structural plywood.
MOR (Modulus of Rupture): Maximum stress before fracture under bending load (MPa)
MOE (Modulus of Elasticity): Ratio of stress to strain within the elastic deformation range, reflecting bending stiffness
Typical Values: High-quality 5-ply furniture plywood: MOR ≥50 MPa, MOE ≥5000 MPa; construction formwork: MOR ≥80 MPa.
4.4 Formaldehyde Emission
Formaldehyde emission is the core indicator of environmental performance, directly affecting indoor air quality. Main test methods include:
| Test Method | Principle | Applicable Standard |
|---|---|---|
| Chamber Method | Specimen placed in climate chamber (23°C/50%RH); air extracted to absorb formaldehyde; spectrophotometric determination | GB/T 17657-2022 |
| Desiccator Method | Specimen suspended in sealed desiccator; absorbing solution absorbs formaldehyde; colorimetric determination | GB/T 17657-2022 |
| Perforator Extraction Method | Formaldehyde extracted from specimen with toluene; then determined | GB/T 17657-2022 (arbitration method) |
China's Wood-Based Panel Environmental Grade Classification (GB 18580-2025):
| Environmental Grade | Formaldehyde Emission (Chamber Method, mg/m³) |
|---|---|
| E1 (Mandatory National Standard) | ≤0.050 |
| E0 | ≤0.025 |
| ENF | ≤0.015 |
4.5 Appearance Grade Assessment
Appearance grades are assessed according to GB/T 9846 based on the following defect items:
Knots (size and quantity of live/dead knots)
Discoloration (oxidation discoloration, mold)
Cracks, fissures
Holes, insect holes
Overlaps (veneer misalignment)
Blisters, wrinkles
Glue contamination (glue bleed-through, glue spots)
V. Common Classifications and Applications of Plywood
5.1 Classification by Bonding Strength and Water Resistance
| Category | Adhesive Type | Water Resistance | Typical Applications |
|---|---|---|---|
| Interior Plywood | Urea-Formaldehyde (UF) | Dry conditions | Furniture, interior decoration |
| Exterior Plywood | Phenolic (PF) | Water-resistant/Weather-resistant | Exterior walls, outdoor furniture |
| Marine Plywood | WBP Phenolic | Boil-proof | Marine vessels, offshore engineering |
5.2 Classification by Face Material
| Type | Characteristics | Main Applications |
|---|---|---|
| Natural Wood Veneer Plywood | Real wood grain, premium texture | High-end furniture, interior decoration |
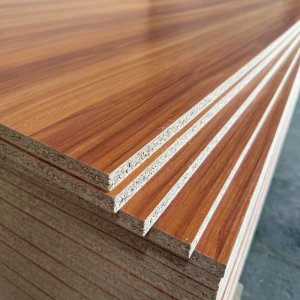
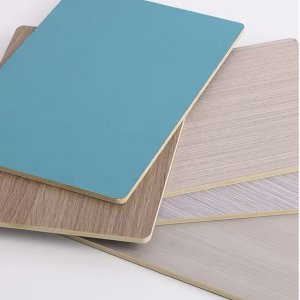
| Melamine-Faced Plywood | Wear-resistant, heat-resistant, rich patterns | Panel furniture, cabinets |
| Film-Faced Plywood (Formwork) | Phenolic film overlay, waterproof and wear-resistant | Concrete formwork |
| Raw (Unfinished) Plywood | Natural substrate color, low cost | Packaging, industrial uses |
5.3 Classification by Application
| Application Field | Core Requirements | Representative Products |
|---|---|---|
| Furniture Manufacturing | Aesthetic appearance, eco-friendly, strong nail-holding | Furniture panels, melamine-faced panels |
| Building Construction | High strength, waterproof, high reuse cycles | Formwork, marine plywood |
| Transportation | Impact resistance, strong weather resistance | Vehicle flooring, carriage panels |
| Industrial Packaging | Cost-effective, reliable strength | Packaging plywood |
| Decoration and Renovation | Attractive patterns, flat surface | Wall paneling, feature wall substrates |
VI. Common Quality Issues and Cause Analysis
6.1 Delamination
Phenomenon: Separation of adhesive layers at board edges or internally; in severe cases, the entire board separates.
Possible Causes:
Substandard adhesive quality or improper formulation
Insufficient glue spread or uneven application
Inadequate hot pressing temperature or pressure preventing complete curing
Excessive veneer moisture content (steam pressure during hot pressing damages adhesive layer)
Adhesive beyond its pot life (using aged adhesive)
Solutions: Strict adhesive incoming inspection, standardized hot pressing process parameters, dynamic monitoring of veneer drying moisture content.
6.2 Blistering
Phenomenon: Localized protrusions on the board surface, hollow or delaminated internally.
Possible Causes:
Temperature rises too quickly in the early stage of hot pressing; internal moisture vaporizes rapidly creating high pressure
Excessive or uneven moisture content in veneers
Trapped air in the mat未能排出
Uneven glue application causing localized glue starvation
Solutions: Use a three-stage temperature curve (preheating → curing → cooling equalization); strictly control veneer moisture content uniformity.
6.3 Warping Deformation
Phenomenon: Board surface twisted, tile-shaped or bowed.
Possible Causes:
Lay-up violates symmetry principle (inconsistent veneer thickness, species, or moisture content on both sides)
Uneven moisture content (one side dry, the other wet)
Excessive sanding disrupting board stress balance
Finished products stacked unevenly or insufficient weight applied
Solutions: Strictly symmetric lay-up, balanced moisture content control, appropriate sanding allowance, finished products stored flat under weight.
6.4 Glue Bleed-Through and Glue Spots
Phenomenon: Adhesive exuding to the board surface, forming hard glue spots that affect finishing.
Possible Causes:
Excessive glue spread or low adhesive viscosity
Uneven veneer thickness (thin areas allow bleed-through)
Excessive hot pressing pressure squeezing out adhesive
Solutions: Precise glue spread control (prefer metering-roll glue spreaders), optimized hot pressing pressure parameters, suitable adhesive viscosity selection.
VII. Technology Development Trends of Plywood
7.1 Green and Environmental Focus
With the implementation of the new national standard GB 18580-2025 and increasing global environmental awareness, formaldehyde-free plywood (ENF/HENF grade) is becoming the mainstream demand. New eco-friendly adhesives such as MDI formaldehyde-free adhesive and soy protein adhesive will see gradually expanding applications.
7.2 Functional Integration
Single-purpose panels are evolving toward multi-functional composite panels: fire resistance, mold resistance, decay resistance, insect resistance, and other functions can be achieved through adhesive additives or veneer pre-treatment. JINDIWOOD can customize multi-functional composite panels according to customer requirements.
7.3 Thin, Light, and High-Strength
By optimizing hot pressing processes, selecting high-strength species, and using advanced adhesive types, mechanical properties are maintained or even improved while reducing board thickness and weight, meeting lightweight application requirements (such as high-speed rail interiors, aircraft interiors, yacht manufacturing).
7.4 Digital Quality Control
Digital monitoring technologies — online thickness detection, X-ray density detection, near-infrared moisture content detection — are replacing traditional manual sampling inspection, achieving 100% quality traceability across all batches and ensuring zero-defect delivery of finished products.

JINDIWOOD · Engineered for Certainty — Crafting every board with core technology, securing every partnership with a commitment to certainty.
This article is an original technical publication by JINDIWOOD. Reproduction must indicate the source.