中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
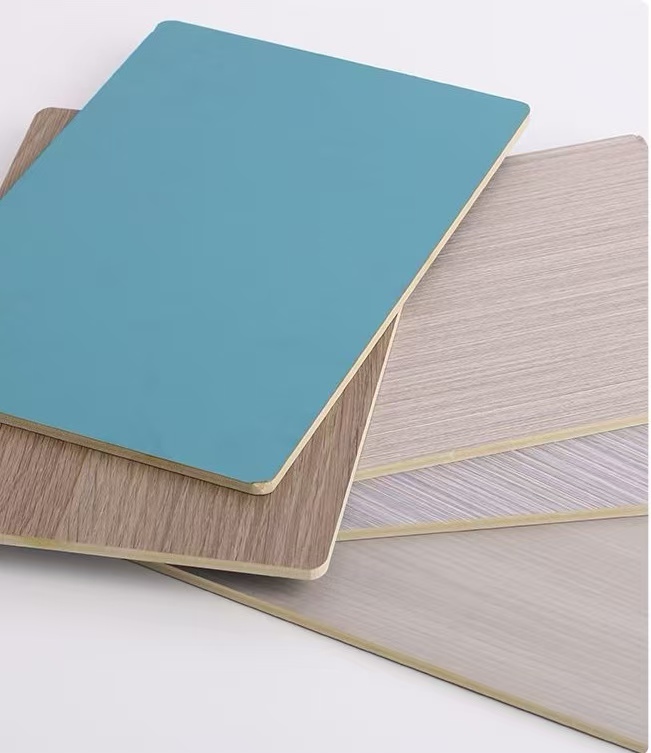
— From Curing Process to Eco-Friendly Finishes, Decoding the New Generation of "Paint-Free Decorative Panels"
I. Basic Concept of Melamine Impregnated Paper
The more professional name for melamine impregnated paper is "Melamine Impregnated Paper" (MIP) , commonly known as "melamine paper," "impregnated paper," or "decorative paper." It is a semi-cured decorative material made by impregnating decorative base paper with melamine resin, followed by drying and cutting.
It is not a finished product in itself, but an intermediate material for wood-based panel decoration. Under high temperature and high pressure, the resin in the paper melts, flows, cross-links, and cures, bonding tightly with the substrate (particleboard, MDF, plywood, etc.) to form a wear-resistant, heat-resistant, stain-resistant, and color-rich decorative protective layer. After this process, ordinary wood-based panels become the melamine-faced panels (commonly known as "eco-boards" or "lacquer-free boards") we see in furniture, cabinets, and flooring.
MIP = Base Paper + Melamine Resin
| Concept | Definition | Form | Use |
|---|---|---|---|
| Decorative Base Paper | Industrial paper made from wood pulp, titanium dioxide, etc., containing no resin itself | Roll paper (like thick cultural paper) | Carrier for printing patterns or providing solid color base |
| Melamine Impregnated Paper | Semi-finished product after base paper is impregnated with resin and dried | Roll paper (resin content approx. 100-200%, hard and brittle, slightly tacky) | Directly used for pressing decorative panels |
Core essence: MIP is a composite of "decorative paper + resin." It carries the pattern (aesthetics) and provides physical protection via cured resin (performance), making it the key material for "lacquer-free" processes.
Industry Status & Scale:
According to the Decorative Paper Committee of the China National Forest Products Industry Association, China's annual production of melamine impregnated paper exceeded 2.8 million tons (approx. 19 billion m²) in 2025, accounting for over 65% of global output, making it the world's largest producer and consumer. Of this, ~55% is used for panel furniture, ~20% for laminate flooring, ~15% for cabinets/bathroom vanities, and ~10% for other decorative uses.
JINDIWOOD, as a board manufacturer, has a deep understanding of paper quality: we use high-standard MIP to ensure excellent decorative effects and physical properties, delivering high-quality, aesthetically pleasing, and durable panels.
II. Classification of Melamine Impregnated Paper
2.1 By Base Paper Type
| Base Paper Type | Function | Weight (g/m²) | Features | Applications |
|---|---|---|---|---|
| Printable Decorative Paper | Carries printed patterns (wood, stone, fabric grain) | 70-100 | Good ink absorption, high opacity, gravure printing (register ≤0.15mm) | Panel furniture, cabinets, wooden doors (rich patterns, mainstream) |
| Solid Color Decorative Paper | Provides single solid colors | 80-120 | Vivid colors, high opacity, strict color control (ΔE≤0.5) | Solid color furniture, office furniture, interior decor (minimalist) |
| Overlay Wear-Resistant Paper | Provides wear resistance (contains Al₂O₃) | 40-60 (thin) / 80-120 (thick) | Contains α-Al₂O₃, wear resistance up to 4000-10000 revolutions | Laminate flooring (core use), high-wear furniture |
| Balancing Paper (Bottom Layer) | Pressed on the bottom to balance stress and prevent warping | 40-60 | No printing, only resin impregnation, for symmetric structure | Laminate flooring, panel furniture (prevents bending) |
| Edgebanding Base Paper | For making edgebanding strips | 60-100 | Printed and impregnated, cut into rolls for edges | Edgebanding strips |
| High-Definition Paper | Special process (coating + high-transparency resin) for clearer patterns | 80-110 | High transparency, fully presents pattern details (especially dark wood grains) | High-end furniture, custom cabinets, luxury display cases |
2.2 By Surface Gloss Level (After Pressing)
| Type | Gloss (GU, 60°) | Features | Style |
|---|---|---|---|
| High-Gloss | ≥85 (up to 95+) | Mirror effect, strong visual impact, but prone to fingerprints, high substrate flatness required | Modern minimalism, luxury, commercial spaces |
| Matt | ≤15 | Soft texture, non-reflective, delicate touch, less fingerprints, more premium | Nordic, Japanese, Neo-Chinese, children's rooms |
| Semi-Gloss (Satin) | 25-50 | Between high-gloss and matt, moderate shine | Simple modern, office furniture |
2.3 By Embossing Type (Synchronized Pores/Register Embossing)
| Embossing Type | Principle | Effect | Cost Level |
|---|---|---|---|
| Synchronized Pores | Press plate texture precisely aligns with printed pattern (deviation ≤0.5mm), matching visual and tactile texture | Extremely realistic, wood grain vessels and stone veins tangible, nearly indistinguishable from real wood/stone | Highest |
| Non-Synchronized (Regular) | Regular geometric patterns (e.g., linen, checkered, leather) not matching printed pattern | Regular texture, rougher feel, suitable for specific styles (e.g., industrial, modern) | Medium |
| No Embossing (Smooth) | Mirror-finished steel plate, completely smooth surface | High-gloss/matt smooth surface, strong modern feel | Medium |
| Deep Embossing (3D, depth ≥0.15mm) | Higher temp and pressure for ≥0.15mm deep texture | Strong tactile feel, wood grain vessels "sunken" into board, prominent 3D effect | High |
2.4 By Environmental Protection Grade
| Grade | Formaldehyde Emission (Chamber Method, mg/m³) | Resin Type | Applications |
|---|---|---|---|
| E1 | ≤0.050 (GB 18580-2025 mandatory) | Standard MF resin | General furniture (non-children, non-bedroom) |
| E0 | ≤0.025 | Low molar ratio MF + formaldehyde scavenger | Mid-to-high end furniture, interior decoration |
| ENF | ≤0.015 | Ultra-low molar ratio resin + efficient scavenger | Children's furniture, bedrooms, hospitals, schools |
| HENF (Zero Added) | ≤0.015 (all items met) | Optimized MUF co-condensation resin (near-zero free formaldehyde) | High-end residential, whole-house customization |
III. Raw Material System of MIP
3.1 Base Paper – The "Gene" of Basic Performance
(Key indicators: basis weight, tensile strength, wet strength, opacity, Cobb value, ash content, smoothness, color difference)
3.2 Melamine Resin – The "Core" of Physical Performance
Melamine resin is a thermosetting resin formed by polycondensation of melamine and formaldehyde under alkaline conditions. It is the fundamental reason why the paper can cure, wear-resist, heat-resist, and stain-resist.
(Key parameters: solid content, viscosity, pH, free formaldehyde content, curing time, M/F ratio. Modifications include urea co-condensation, caprolactam/diethylene glycol addition, formaldehyde scavengers, nano-SiO₂/Al₂O₃ addition.)
IV. Production Process of MIP
Process Flow:Base paper unwinding → Resin impregnation (1st dip) → Metering rollers → 1st drying → 2nd impregnation (top coat) → 2nd metering → 2nd drying → Cooling → Cutting/Winding → QC → Finished rolls
Key Steps:
1st Impregnation: Paper passes through resin bath (25-35°C) at 10-40m/min. Resin pick-up: 60-100% of base paper weight.
Metering: Squeezes excess resin for uniform distribution.
1st Drying: 3 zones (80-120°C / 120-160°C / 100-130°C). Residual volatiles controlled at 5-8%; pre-cure degree: 20-40%.
2nd Impregnation (Top Coat): Applies higher solids resin (50-60%) on the printed side, adding wear-resistant agents (Al₂O₃), anti-fingerprint agents, etc. Top coat weight: 10-25g/m² (dry resin).
2nd Drying & Cooling: Final volatiles 5-7%, cooled to room temperature.
Cutting & Winding: Cut to 1220/1240mm widths, wound with anti-stick interleaving paper, packed in aluminum foil composite bags.
Key QC Points: Resin content, volatiles, pre-cure degree, appearance, width, warping.
V. Core Technical Specifications
5.1 Resin Content (Impregnation Rate)
Printable paper: 120-160% (light) / 130-180% (dark)
Solid color: 130-180%
Overlay paper: 180-250%
Balancing paper: 100-150%
5.2 Volatile Content
4-6% (fast pressing, flooring)
6-8% (conventional, furniture/cabinets - most common)
8-10% (thick boards or low-temp pressing)
5.3 Pre-Cure Degree
20-40% is optimal. Too high = poor adhesion; too low = blistering.
5.4 Flowability
Measured at 150°C; typically 120-160mm diagonal expansion.
5.5 Wear Resistance (Overlay Paper Only)
AC1: ≥2000 revs (bedroom/study)
AC2: ≥3000 revs (living room)
AC3: ≥4000 revs (office/shop)
AC4: ≥6000 revs (mall/restaurant)
AC5: ≥8000 revs (airport/exhibition)
VI. Lamination (Pressing) Process
6.1 Parameters
Pressing Temperature: 180-210°C
Pressing Pressure: 2.5-4.0 MPa
Pressing Time: 8-15s (short-cycle) / 30-60s (long-cycle)
6.2 Common Methods
LPL (Low Pressure Laminate): 185-200°C, 2.5-3.5 MPa, 8-15s → panel furniture, cabinets.
HPL (High Pressure Laminate): 150-180°C, 4.0-6.0 MPa, 30-60s → fireproof boards, high-wear.
Continuous Laminate (CPS) → mass production (flooring, large panels).
6.3 Press Plate Selection
Mirror plate → high-gloss (≥85GU)
Matt/Satin plate → matte (≤15GU)
Synchronized plate → realistic wood/stone
Regular pattern plate → industrial/modern
Deep 3D plate → antique/3D effect
VII. Common Quality Myths & Facts
(Debunks: brighter = better; higher wear resistance = always better; thicker paper = better; melamine panels are always unhealthy.)
VIII. Comparison with Other Decorative Materials
(Compared with PVC film, wood veneer, paint coating, HPL across: hardness, wear resistance, heat resistance, stain resistance, pattern variety, eco-grade potential, cost, realism.)
IX. Future Technology Trends
9.1 High Realism (Synchronized + Digital Printing)
Registration accuracy improves from ±1.0mm to ±0.3mm.
Digital printing (≥1200dpi, 50-100m/min) enables small-batch customization.
3D tactile depth ≥0.25mm.
9.2 Functionalization
Antibacterial/Antiviral (Ag⁺/ZnO, ≥99.9% efficacy).
Anti-fingerprint (fluoropolymer additives).
Thermochromic/Photochromic.
9.3 Eco-friendly & Low-Carbon
Bio-based melamine resin (lignin/tannin replacing 10-30% formaldehyde).
Low-temperature curing resin (140-160°C, saving 15-25% energy).
Biodegradable additives (PCL).
9.4 Digital & Smart Production
AI defect detection (CNN + cameras, 0.1mm precision, ≥95% accuracy).
Digital recipe management (full traceability).
Flexible production (color changeover from 2-4h to 15-30min).
JINDIWOOD · Engineered for Certainty
Every precisely impregnated and perfectly bonded sheet of decorative paper paints a certain future for the aesthetics and durability of your home.