中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
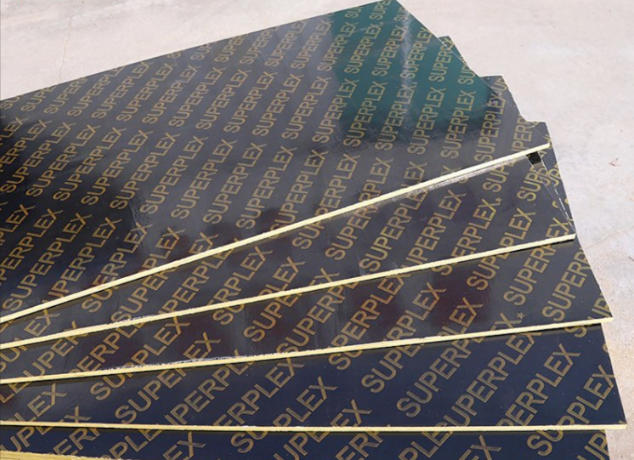
I. Basic Concept of Formwork Plywood
Formwork plywood, also known as concrete formwork plywood, construction formwork, or film faced plywood, is a special plywood designed and manufactured for cast-in-place concrete structure construction. It uses wood-based plywood as the substrate and, through special adhesives and surface treatment processes, gives the panel high strength, waterproofness, wear resistance, and multiple reusability, serving as the mold panel for concrete pouring and forming.
In modern construction, formwork engineering is a key stage that determines concrete forming quality, construction speed, and project cost. As the core panel material of the formwork system, plywood quality directly affects:
The flatness and smoothness of the concrete surface (whether a "fair-faced concrete" effect is achieved)
The number of formwork reuses (directly affecting construction cost)
Construction safety (the stability basis of the formwork support system)
Project progress (matching of formwork removal time with concrete curing cycle)
Key Data: In high-rise buildings and large infrastructure construction, formwork engineering costs typically account for 30-50% of the total cost of concrete structure engineering, with labor accounting for about 40-50%. The choice of high-quality formwork has an extremely significant impact on overall project benefits.
II. Classification and Grading of Formwork Plywood
2.1 Classification by Surface Treatment
This is the most important product classification dimension for formwork plywood.
| Type | Surface State | Characteristics | Reuse Times | Applications |
|---|---|---|---|---|
| Untreated panel (raw) | Natural substrate color, surface uncoated | Lowest cost, easy to stick with cement, difficult to clean, rough surface | 3-5 times | Low-requirement temporary works, blinding formwork |
| Coated panel (resin coating) | Surface coated with phenolic or melamine resin | Relatively smooth surface, easy to clean, certain waterproofness | 8-12 times | General industrial and civil buildings |
| Film faced panel (impregnated film paper) | Surface covered with phenolic resin impregnated strong kraft paper or special film paper | Extremely smooth surface, wear-resistant and waterproof, can achieve mirror effect | 20-30 times (premium) | High-rise buildings, fair-faced concrete, large bridges |
Film paper color of film faced panels: Black, brown, and red are common in China. Color mainly distinguishes different film paper materials and brands; it does not affect physical performance. The film of a high-quality film faced panel should bond tightly to the substrate and not peel or fall off during repeated use.
2.2 Classification by Bonding Strength and Water Resistance Grade (GB/T 17656-2018)
| Water Resistance Grade | Adhesive Type | Performance Characteristics | Applicable Environment |
|---|---|---|---|
| Class I (high water resistance) | Phenolic resin adhesive (PF) | Can withstand boiling water immersion and long-term humid environments, bonding strength ≥0.70 MPa | Outdoor works, long-term humid environments, hydraulic structures |
| Class II (water resistant) | Melamine modified urea-formaldehyde adhesive (MUF) | Resists cold water immersion; short-term moisture does not affect bonding performance | General construction projects, indoor construction |
| Class III (non-water resistant) | Urea-formaldehyde adhesive (UF) | Only suitable for dry environments; easily delaminates when exposed to water | Non-load-bearing or indoor short-term formwork |
JINDIWOOD Formwork Plywood Standard: All core products use phenolic resin adhesive (PF/WBP grade), with water resistance Class I, capable of withstanding the high-temperature and high-humidity environment generated by cement hydration heat during concrete pouring, ensuring the formwork does not delaminate or separate during repeated use.
2.3 Classification by Wood Species
| Wood Species | Density (kg/m³) | Characteristics | Applications |
|---|---|---|---|
| Poplar core | 450-550 | Light and soft, economical, moderate reuse times | Low- and mid-rise buildings, general civil construction |
| Pine core | 500-600 | Straight grain, contains natural resin, good bonding performance | High-rise buildings, bridges |
| Eucalyptus core | 550-650 | Relatively high strength, moderate density, good water resistance | Heavy structures, high-reuse projects |
| Birch core | 600-700 | Dense material, high strength, fine surface | Premium fair-faced concrete formwork |
| Mixed hardwood core | 550-650 | Balanced overall performance, high cost-performance | General-purpose construction formwork |
III. Core Technical Requirements for Formwork Plywood
3.1 Mechanical Performance Requirements (GB/T 17656-2018)
Formwork plywood must withstand the lateral pressure of concrete during pouring (related to pouring speed, concrete slump, and pouring height, usually within the range of 20-100 kN/m²), so it must have excellent mechanical performance.
| Technical Indicator | Unit | National Standard Requirement | JINDIWOOD Standard |
|---|---|---|---|
| Modulus of Rupture (MOR) | MPa | ≥ 40 (parallel) / ≥ 30 (perpendicular) | ≥ 50 (parallel) |
| Modulus of Elasticity (MOE) | MPa | ≥ 6000 (parallel) / ≥ 4500 (perpendicular) | ≥ 7500 (parallel) |
| Bonding strength | MPa | ≥ 0.70 | ≥ 1.0 |
| Moisture content | % | 6-14 | 8-12 |
| Thickness tolerance | mm | ±0.8 | ±0.5 |
| Warping degree | % | ≤ 1.0 | ≤ 0.5 |
3.2 Physical Performance Requirements
Surface wear resistance: The phenolic film on the surface of film faced panels must withstand friction and alkaline erosion from multiple concrete pours. It is assessed by the Taber abrasion test, measured as mass loss per 100 revolutions (g/100r). The mass loss of a high-quality film faced panel should be ≤0.08 g/100r.
Surface impact resistance: Formwork withstands impacts from aggregate falling and vibrator contact during construction. It is measured by the falling ball impact test—a steel ball is dropped from a certain height onto the panel surface to check whether the film layer cracks or peels. JINDIWOOD film faced panels can withstand the impact of a 500 g steel ball dropped from 500 mm without film layer damage.
Alkali resistance: Concrete pH is usually between 12-13 (strongly alkaline), and the formwork surface must resist alkaline corrosion. Phenolic resin film has good alkali resistance; after immersion in saturated calcium hydroxide solution for 72 hours, the surface shows no blistering or discoloration.
3.3 Dimensional Specifications
Formwork plywood dimensions vary according to construction habits in different countries and regions:
| Specification | Dimensions (mm) | Main Market |
|---|---|---|
| 4×8 ft (standard) | 1220 × 2440 | Global |
| 3×6 ft | 1830 × 915 | China and Southeast Asia |
| 4×10 ft | 1220 × 3050 | Europe, Middle East |
| 4×12 ft | 1220 × 3660 | North America large projects |
Thickness specifications: Common thicknesses for formwork plywood are 12 mm, 14 mm, 15 mm, 18 mm, 20 mm, 21 mm, 24 mm, and 27-30 mm. Among them, 15 mm and 18 mm are mainstream market specifications. The choice of panel thickness must comprehensively consider concrete lateral pressure and support spacing—situations with high lateral pressure or large support spacing require thicker formwork to prevent excessive deformation of the formwork panel during pouring.
IV. Production Process Characteristics of Formwork Plywood
The production process of formwork plywood is similar to ordinary plywood (see the previous article "Plywood Production Complete Guide"), but due to the requirements of construction scenarios for high strength, high waterproofness, and high flatness, formwork plywood has significantly higher technical standards in three aspects: veneer grade, adhesive system, and hot pressing process.
4.1 Raw Material and Veneer Requirements
Higher veneer grade:
Surface veneers of formwork plywood must be free of knots, holes, and cracks to avoid surface defects or grout leakage during concrete pouring
Core veneers have higher splicing quality requirements; overlaps or gaps are not allowed
Stricter veneer drying:
Formwork plywood requires higher moisture content uniformity than ordinary furniture panels (within ±1.5%), because uneven moisture content directly causes panel warping after hot pressing, affecting formwork flatness
Drying temperature control is more precise to avoid excessive surface hardening that affects adhesive penetration
4.2 Adhesive System (Core of Construction Formwork)
The adhesive for formwork plywood is mainly phenolic resin adhesive (PF), with some products using melamine modified urea-formaldehyde adhesive (MUF) or mixed adhesives.
Special formula of phenolic resin adhesive (PF) for construction formwork:
Solid content: 45-55% (higher than ordinary PF adhesive, ensuring sufficient bonding strength)
Viscosity: 300-800 cps (25°C), ensuring coating uniformity
pH value: 10-12 (alkaline system, matching the curing characteristics of phenolic resin)
Curing temperature: 140-160°C (higher than 120-140°C for urea-formaldehyde adhesive)
Pot life: 4-8 hours (25°C); must be used within the pot life
Phenolic adhesive coating amount: The coating amount for formwork plywood is usually higher than ordinary plywood, at 220-280 g/m² (double-sided total), ensuring the adhesive layer does not fail under harsh conditions of high temperature, high humidity, and repeated reuse.
4.3 Hot Pressing Process (High Requirements Determine High Quality)
The hot pressing process parameters of formwork plywood are higher than ordinary plywood to ensure product density and water resistance:
| Process Parameter | Ordinary Plywood | Formwork Plywood |
|---|---|---|
| Hot pressing temperature | 120-140°C | 140-160°C |
| Unit pressure | 1.0-1.8 MPa | 1.8-2.5 MPa |
| Hot pressing factor (min/mm) | 0.8-1.0 | 1.2-1.5 |
| Pressure holding time | Shorter | Longer |
Higher hot pressing temperature and longer pressure holding time ensure sufficient curing and crosslinking of the phenolic resin adhesive, giving formwork plywood excellent water resistance and bonding strength, but also mean higher energy consumption and production costs.
4.4 Film Facing Process (Key Process of Film Faced Panels)
Film faced panels are made by applying a layer of phenolic resin impregnated film paper onto the plywood substrate after hot pressing, then performing a second hot pressing (or one-step hot pressing with the substrate).
Technical points of film facing process:
Film paper selection: High-quality film faced panels use high-strength kraft paper impregnated with phenolic resin; the impregnated resin content is usually 40-55% (based on raw paper weight), with volatile content controlled at 5-8%
Film paper bonding: The impregnated film paper is covered on the substrate surface and bonded at 150-170°C and 1.5-2.5 MPa pressure
Film paper thickness: Typical value 0.12-0.25 mm. Too thin—poor wear resistance, low reuse times; too thick—increased cost, and possible film cracking due to differences in thermal expansion coefficients
Quality inspection of film faced panels:
Peel strength between film layer and substrate ≥0.5 N/mm
Film surface free of bubbles, wrinkles, and missed coating
Flowability of impregnated film paper must reach 125-155 mm (115°C), ensuring sufficient resin melting and flow during hot pressing to fill surface micropores of the substrate
V. Engineering Applications and Selection of Formwork Plywood
5.1 Selection by Project Type
| Project Type | Recommended Product | Recommended Thickness | Expected Reuse Times |
|---|---|---|---|
| Low-rise residential (≤6 floors) | Coated panel/film faced panel | 15 mm | 8-15 times |
| Mid- to high-rise residential (7-18 floors) | High-quality film faced panel | 18 mm | 20-25 times |
| Super high-rise (≥30 floors) | High-strength film faced panel (hardwood core) | 18-20 mm | 25-30 times |
| Bridges/viaducts | High-strength film faced panel | 18-24 mm | 15-25 times |
| Fair-faced concrete | Premium film faced panel (high gloss) | 18 mm | 20-25 times |
| Tunnels/culverts | Curved special film faced panel | 15-18 mm | 10-15 times |
| Nuclear power plants/dams | Special high-strength panel | 24-30 mm | 30+ times |
5.2 Special Requirements for Fair-Faced Concrete Formwork
Fair-faced concrete refers to a construction process that is formed in one pass, without any external decoration, directly using the natural concrete surface as the finish. Its requirements for formwork are extremely demanding:
| Requirement Dimension | Specific Standard |
|---|---|
| Surface flatness | Measured with 2 m straightedge, deviation ≤1.5 mm |
| Surface smoothness | Can achieve mirror effect, no bubbles, no pinholes, no repair marks |
| Joint precision | Formwork joint ≤0.5 mm, ensuring no grout leakage |
| Surface texture | Formwork surface requires extremely fine texture (similar to fine sandpaper), giving the concrete surface a dense, uniform texture |
Key points for selecting fair-faced concrete formwork:
Use premium birch or pine core film faced panels with extremely high surface flatness
The formwork surface should have moderate roughness (Ra 3.2-6.3 μm)—neither too smooth (insufficient release agent adhesion, bubbles difficult to discharge) nor too rough (poor concrete surface texture)
The number of formwork reuses must be precisely controlled—after exceeding the recommended reuse times, surface performance declines and timely replacement is required
5.3 Key Points for Matching Use of Construction Formwork
Use of release agent:
High-quality formwork must be used with a suitable release agent (water-based or oil-based), with moderate dosage:
Too little: concrete sticks to formwork, difficult removal, surface defects
Too much: oil spots or color differences appear on concrete surface, affecting finish effect
Formwork support spacing:
Support spacing is closely related to formwork thickness and concrete lateral pressure. Taking 18 mm film faced panel as an example, under conventional pouring speed (2-3 m/h) and slump (120-160 mm), secondary joist spacing is usually 200-300 mm, and primary joist spacing is 600-900 mm. In actual projects, it must be determined by calculation to ensure formwork deformation does not exceed L/400 (L is support span).
Formwork maintenance and storage:
Clean concrete residue from the panel surface promptly after use to avoid scratching the film layer with hard objects
Store horizontally with wood blocks underneath, avoiding moisture and direct sunlight
Long-term storage areas should have rain and moisture protection measures and maintain ventilation
VI. Quality Identification of Formwork Plywood
6.1 Appearance Identification
| Inspection Item | High-Quality Formwork Performance | Low-Quality Formwork Performance |
|---|---|---|
| Surface film layer | Smooth and uniform, no bubbles, dents, or scratches | Pinholes, pits, film peeling at edges |
| Panel edge | Clean cut, visible dense adhesive layer, no voids | Porous cut, gaps or cracks, visible bubbles in adhesive layer |
| Panel flatness | No obvious wave patterns under light | Visible waves with naked eye |
| Marking | Brand, thickness, grade, etc. clear and complete | Blurred or no marking |
6.2 Physical Testing
Boiling water test: Place formwork specimens in boiling water for 4 hours, remove and dry in a 63±3°C oven for 20 hours, then boil again for 4 hours. Observe whether specimens show delamination, separation, or blistering. High-quality formwork plywood should show no obvious changes, with bonding strength retention ≥70%.
Hot-cold cycle test: Specimens are immersed alternately in 100°C boiling water and 0°C cold water for 1 hour each (one cycle each time). After 10 cycles, high-quality formwork should show no adhesive layer cracking.
Simple on-site identification methods:
Tap and listen: Lightly tap different positions on the panel with a hard object; clear and consistent sound indicates good quality; dull or hollow sound may indicate internal delamination
Water drop test: Drop a few drops of water on the film faced panel surface and observe after 2 hours: water droplets remaining bead-shaped and not penetrating is good; if water droplets penetrate quickly or water marks appear around them, film quality is poor
Fingernail scratch test: Scratch the film surface firmly with a fingernail; no scratches or slight scratches are good; obvious scratches indicate insufficient film hardness
6.3 Comparison of Key Indicator Data
| Quality Grade | Reuse Times | Price (Reference) | Applicable Projects |
|---|---|---|---|
| Low-end untreated panel | 3-5 times | Economical | Blinding, temporary works |
| Ordinary coated panel | 8-12 times | Medium | General buildings |
| Standard film faced panel (poplar core) | 15-20 times | Medium-high | High-rise residential |
| High-quality film faced panel (hardwood core) | 25-30 times | High | Super high-rise, fair-faced concrete |
| Premium film faced panel (birch core) | 30+ times | High | Key projects, fair-faced concrete |
VII. Factors Affecting the Reuse Times of Formwork Plywood
The reuse times of formwork plywood is a core indicator of its economic efficiency. The single-use cost of high-quality formwork plywood is far lower than that of low-priced formwork, with better overall economic benefits.
| Influencing Factor | Impact on Reuse Times |
|---|---|
| Surface film quality | Film paper resin content and hot pressing curing degree determine wear resistance and alkali resistance, directly affecting release effect and service life |
| Bonding strength | Determines whether the formwork delaminates during repeated bending, vibration, and knocking—delamination means scrapping |
| Core material quality | Hardwood core (birch, eucalyptus) has higher compressive strength than softwood core (poplar), reducing panel failure caused by compression |
| Construction operation | Rough formwork removal, hard object scratching, and failure to clean residual grout greatly reduce reuse times |
| Storage conditions | Open-air stacking, rain exposure, and uneven ground accelerate formwork aging and deformation |
| Concrete characteristics | High-slump concrete exerts greater lateral pressure and stronger alkalinity on formwork, with more significant erosion effects |
Measured reuse data of JINDIWOOD formwork plywood:
Standard film faced panel (poplar core, 18 mm): 20-25 times (under normal construction conditions)
High-strength film faced panel (pine core, 18 mm): 25-30 times
Premium film faced panel (birch core, 18 mm): 30-35 times
VIII. Common Quality Problems of Formwork Plywood
8.1 Panel Surface Blistering
Phenomenon: Bubbles of varying sizes appear on the surface of film faced panels; in severe cases, the film layer bulges or detaches.
Causes:
Temperature too high or hot pressing time insufficient during film facing, so volatiles in the film paper do not fully escape
Substrate moisture content too high; water vapor accumulates under the film layer during hot pressing
Film paper resin content too low or too high, improper flowability control
Solutions: Strictly control substrate moisture content (≤12%), optimize film facing hot pressing process curve (use stepped temperature rise method), control impregnated film paper volatile content within 5-8%.
8.2 Film Peeling/Delamination
Phenomenon: The film layer peels off from the substrate surface, or the adhesive layer inside the substrate cracks.
Causes:
Substrate surface not clean enough before film facing (dust, grease, or sanding powder residue)
Insufficient film paper resin content or poor compatibility between resin and substrate
Frequent scratching by hard objects during reuse, or pry bars directly acting on the panel surface during formwork removal
Long-term alkaline erosion of concrete causes adhesive layer aging
Solutions: Remove panel surface dust with high-pressure air or vacuum before film facing, select suitable matching scheme of film paper and adhesive type, standardize construction operations (strictly prohibit violent formwork removal), reapply surface protective agent after a certain number of reuses.
8.3 Panel Surface Pitting/Not Smooth
Phenomenon: Concrete surface is rough, with tiny pits or pores.
Causes:
Formwork surface itself has uneven roughness or sanding marks
Release agent applied unevenly, forming local sticking
Dust or oil stains on film faced panel surface not cleaned before pouring
Solutions: Select high-quality film faced panels with uniform surface roughness, apply release agent evenly by spraying, blow the panel surface with compressed air before pouring after formwork installation.
8.4 Warping Deformation
Phenomenon: The formwork is bent or twisted overall, unable to fit tightly with the support system, resulting in loose joints and grout leakage.
Causes:
Improper formwork storage (vertical placement or uneven ground)
One side exposed to sun for a long time while the other side is humid, forming a moisture content gradient
Assembly not strictly symmetrical during hot pressing, internal stress not fully released
Insufficient curing time, excessive residual stress
Solutions: Store horizontally, place wood blocks underneath with uniform spacing, curing time not less than 72 hours, turn over promptly after reuse.
IX. Technical Development Trends of Formwork Plywood
9.1 High Reuse and Long Life
By optimizing core wood species combinations, improving phenolic resin formulas, and using thicker and denser film paper, the reuse times of formwork can break through 40-50 times, further reducing single-use costs. Advanced technology directions include nano-modified phenolic film and fiber-reinforced film layers.
9.2 Lightweighting
Under the premise of ensuring strength, by adjusting core structure (such as using low-density high-strength wood species or hollow composite structures), reduce formwork weight per unit area (from conventional 50 kg for 18 mm panel to 35-40 kg), facilitating worker operation and installation and reducing construction labor intensity.
9.3 Digitalization and Intelligence
RFID chip embedding: Each formwork panel is embedded with an RFID tag to record reuse times, project usage, maintenance records, etc., achieving full life cycle management
Intelligent monitoring: Integrate strain sensors and pressure sensors into the formwork system to monitor lateral pressure and formwork deformation in real time during concrete pouring, providing data support for construction safety
9.4 Green and Environmental Protection
Develop bio-based phenolic resin (using lignin, tannin, etc. to replace part of petrochemical raw materials) to reduce carbon footprint
Promote recyclable formwork systems (standardized dimensions for cross-project reuse)
After formwork reaches the end of its service life, it can be crushed and used as biomass fuel or recycled panel raw material
Construction Plywood Frequently Asked Questions (FAQ) — Summary
Q1: What is construction plywood? How important is it in construction projects?
A: Construction plywood, also called concrete formwork plywood, building formwork, or film-faced plywood, is a special plywood designed and manufactured for cast-in-place concrete structures. It uses wood plywood as the substrate and, through special adhesives and surface treatment processes, gives the panel high strength, water resistance, abrasion resistance, and multiple reuse capability. It is used as the formwork panel for concrete casting and molding.
In high-rise buildings and large infrastructure projects, formwork costs typically account for 30–50% of the total cost of concrete structure works, and labor accounts for about 40–50%. Formwork quality directly affects concrete surface flatness and finish, formwork reuse cycles, construction safety, and project schedule.
Q2: How is construction plywood classified by surface treatment? What are the reuse cycles and applications?
A: By surface treatment, construction plywood is mainly divided into three categories:
Raw board (untreated): Lowest cost, prone to mortar adhesion, difficult to clean, rough surface; 3–5 reuse cycles. For low-requirement temporary works, leveling course formwork, etc.
Resin-coated board: Surface coated with a phenolic or melamine resin layer; relatively smooth, easy to clean, with some water resistance; 8–12 reuse cycles. For general industrial and civil buildings.
Film-faced plywood: Surface covered with strong kraft paper impregnated with phenolic resin or special film paper; extremely smooth, wear-resistant and waterproof, capable of achieving a mirror effect; high-quality products: 20–30 reuse cycles. For high-rise buildings, fair-faced concrete, and large bridges.
Common film colors include black, brown, and red; they mainly distinguish film material and brand and do not affect physical performance. High-quality film-faced plywood should have film tightly bonded to the substrate, without peeling or detachment after repeated use.
Q3: How is construction plywood classified by bonding strength and water resistance class?
A: According to GB/T 17656-2018, water resistance classes are:
Class I (high water resistance): Phenolic resin adhesive (PF); withstands boiling water immersion and long-term humid environments; bonding strength ≥0.70 MPa. For outdoor works, long-term humid environments, and hydraulic structures.
Class II (water-resistant): Melamine-modified urea-formaldehyde adhesive (MUF); withstands cold water immersion; short-term moisture does not affect bonding performance. For general construction works and indoor construction.
Class III (non-water-resistant): Urea-formaldehyde adhesive (UF); only for dry environments; easily delaminates when exposed to water. For non-load-bearing or short-term indoor formwork.
JINDIWOOD construction plywood core products all use phenolic resin adhesive (PF/WBP grade), with Class I water resistance. They withstand the high-temperature and high-humidity environment generated by cement hydration heat during concrete casting, ensuring no delamination or separation after repeated use.
Q4: How is construction plywood classified by wood species? What are the characteristics of each?
A: By core wood species, common classifications are:
Poplar core: Density 450–550 kg/m³; light and soft, economical, moderate reuse cycles. For low- and mid-rise buildings and general civil construction.
Pine core: Density 500–600 kg/m³; straight grain, natural resin content, good bonding performance. For high-rise buildings and bridges.
Eucalyptus core: Density 550–650 kg/m³; relatively high strength, moderate density, good water resistance. For heavy structures and high-reuse projects.
Birch core: Density 600–700 kg/m³; dense material, high strength, fine surface. For high-end fair-faced concrete formwork.
Mixed hardwood core: Density 550–650 kg/m³; balanced overall performance, high cost-performance. For general-purpose construction formwork.
Q5: What are the core mechanical and physical technical requirements for construction plywood?
A: Taking GB/T 17656-2018 as an example, core indicators include:
Modulus of rupture (MOR): National standard ≥40 MPa (along grain) / ≥30 MPa (cross grain); JINDIWOOD ≥50 MPa (along grain).
Modulus of elasticity (MOE): National standard ≥6000 MPa (along grain) / ≥4500 MPa (cross grain); JINDIWOOD ≥7500 MPa (along grain).
Bonding strength: National standard ≥0.70 MPa; JINDIWOOD ≥1.0 MPa.
Moisture content: National standard 6–14%; JINDIWOOD 8–12%.
Thickness tolerance: National standard ±0.8 mm; JINDIWOOD ±0.5 mm.
Warping degree: National standard ≤1.0%; JINDIWOOD ≤0.5%.
In terms of physical performance, high-quality film-faced plywood should have a Taber abrasion mass loss ≤0.08 g/100r; withstand impact from a 500 g steel ball dropped from 500 mm without damaging the film layer; and show no blistering or discoloration after 72 hours of immersion in saturated calcium hydroxide solution.
Q6: What special requirements does the production process of construction plywood have compared with ordinary plywood?
A: The production process is similar to ordinary plywood, but requirements are higher in veneer grade, adhesive system, and hot-pressing process:
Veneer requirements: Surface veneer free of knots, holes, and cracks; core splicing not allowed to have overlaps or gaps; moisture content uniformity controlled within ±1.5%.
Adhesive system: Mainly phenolic resin adhesive (PF); solid content 45–55%, viscosity 300–800 cps (25°C), pH 10–12, curing temperature 140–160°C, pot life 4–8 hours; glue spread 220–280 g/m² (double sides).
Hot-pressing process: Hot-pressing temperature 140–160°C, unit pressure 1.8–2.5 MPa, hot-pressing factor 1.2–1.5 min/mm, longer holding time.
Film-facing process: High-quality film-faced plywood uses high-strength kraft paper impregnated with phenolic resin; impregnated resin content 40–55%, volatile content 5–8%, bonding temperature 150–170°C, pressure 1.5–2.5 MPa, film thickness 0.12–0.25 mm, peel strength ≥0.5 N/mm.
Q7: How is construction plywood selected for projects?
A: Recommended selection by project type:
Low-rise residential (≤6 floors): Resin-coated board / film-faced plywood, 15 mm, expected 8–15 reuse cycles.
Mid- and high-rise residential (7–18 floors): High-quality film-faced plywood, 18 mm, expected 20–25 reuse cycles.
Super high-rise (≥30 floors): High-strength film-faced plywood (hardwood core), 18–20 mm, expected 25–30 reuse cycles.
Bridges / elevated roads: High-strength film-faced plywood, 18–24 mm, expected 15–25 reuse cycles.
Fair-faced concrete: Premium film-faced plywood (high gloss), 18 mm, expected 20–25 reuse cycles.
Tunnels / culverts: Special curved-surface film-faced plywood, 15–18 mm, expected 10–15 reuse cycles.
Nuclear power plants / dams: Special high-strength board, 24–30 mm, expected 30+ reuse cycles.
Q8: What special requirements apply to fair-faced concrete formwork?
A: Fair-faced concrete is a construction process in which the concrete surface is formed in one operation, without any external finishing, and directly serves as the finished surface. Requirements for formwork are extremely strict:
Surface flatness: Measured with a 2 m straightedge, deviation ≤1.5 mm.
Surface finish: Can achieve a mirror effect, with no bubbles, sand holes, or repair marks.
Joint precision: Formwork joint gap ≤0.5 mm, ensuring no mortar leakage.
Surface texture: The formwork surface should have a very fine texture, giving the concrete a dense and uniform appearance.
Selection points: Use premium birch or pine core film-faced plywood; surface roughness should be Ra 3.2–6.3 μm; reuse cycles must be precisely controlled, and the panel should be replaced promptly after exceeding the recommended number.
Q9: How can the quality of construction plywood be identified? What simple on-site methods are available?
A: Quality identification can be based on appearance, physical tests, and simple on-site methods:
Appearance: High-quality formwork has a smooth, uniform film layer without bubbles, depressions, or scratches; clean-cut edges with dense adhesive layers; flat surface without obvious waves; clear and complete markings.
Boiling water test: Boil the specimen for 4 hours, dry at 63 ± 3°C for 20 hours, then boil again for 4 hours. High-quality board shows no obvious change, with bonding strength retention ≥70%.
Thermal cycling test: Immerse in 100°C boiling water and 0°C cold water for 1 hour each as one cycle. After 10 cycles, high-quality formwork should show no adhesive layer cracking.
Simple on-site methods: Tap test: clear and consistent sound indicates good quality; water-drop test: water drops remain bead-shaped and do not penetrate; fingernail scratch test: no obvious scratches indicate sufficient film hardness.
Q10: What factors affect the reuse cycles of construction plywood? What are the common quality problems and technical trends?
A: The main factors affecting reuse cycles include: surface film quality, bonding strength, core quality, construction operation, storage conditions, and concrete characteristics. JINDIWOOD measured reuse data: standard film-faced plywood (poplar core, 18 mm) 20–25 cycles; high-strength film-faced plywood (pine core, 18 mm) 25–30 cycles; premium film-faced plywood (birch core, 18 mm) 30–35 cycles.
Common quality problems include: surface blistering, film peeling/delamination, pitting/rough surface, and warping/deformation. Solutions include strictly controlling substrate moisture content, optimizing the film-facing hot-pressing curve, standardizing construction operations, and horizontal storage with rain and moisture protection.
Technical trends include:
High reuse and long service life: Aiming for 40–50 cycles, using nano-modified phenolic films and fiber-reinforced film layers.
Lightweighting: Reducing 18 mm board weight from the conventional 50 kg to 35–40 kg.
Digitalization and intelligence: RFID chip embedding, strain sensors, and pressure sensors for real-time monitoring.
Green and environmental protection: Bio-based phenolic resins, recyclable formwork systems, and end-of-life use as biomass fuel or recycled board raw material.
JINDIWOOD · Engineered for Certainty — Every piece of formwork plywood carries the certainty promise of engineering safety.
This article is an original technical article by JINDIWOOD. Reproduction must indicate the source.