中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
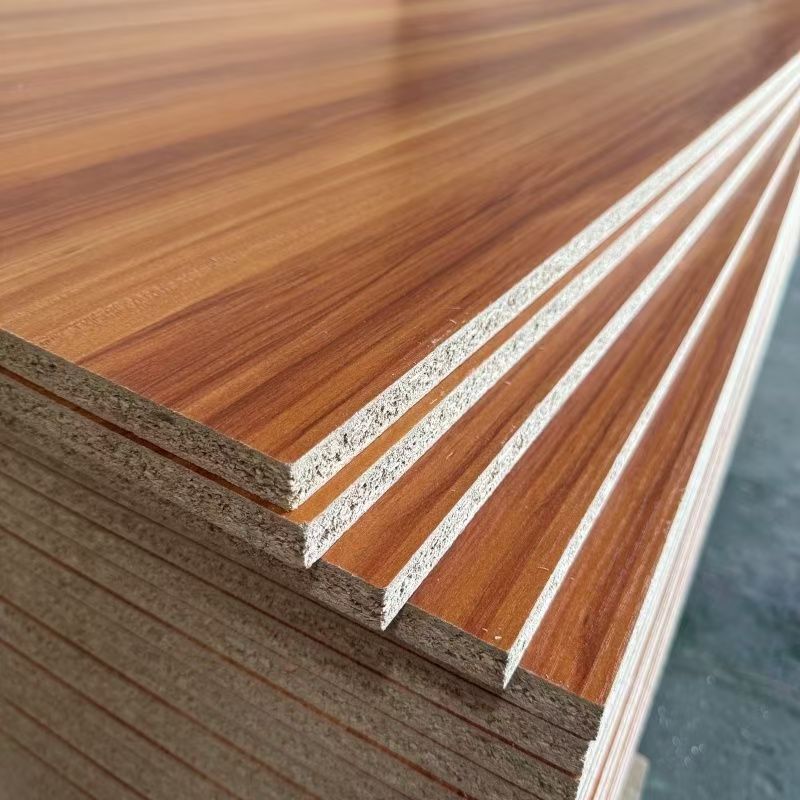
I. Basic Concept of Particleboard
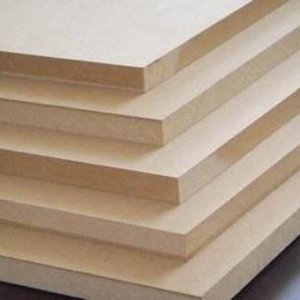
Particleboard (also known as chipboard or bagasse board when using sugarcane bagasse as raw material) is an engineered wood panel manufactured from wood or other plant fiber raw materials processed into particles (wood shavings, sawdust, wood chips, etc.), which are dried, mixed with adhesives and additives, and then hot-pressed at high temperature.
The invention of particleboard dates back to the mid-19th century in Germany, but it was not until the 1940s that truly industrial-scale production was achieved. After more than eighty years of technological development and continuous iteration, particleboard has become one of the world's largest-volume and most widely used engineered wood products — in 2025, global annual particleboard production exceeded 110 million cubic meters, accounting for more than 45% of total engineered wood production.
Core Essence: The manufacturing logic of particleboard is "utilizing inferior materials and reorganizing particles" — recombining waste particles (sawdust, shavings, offcuts, branchwood, etc.) from traditional wood processing into standardized panels using adhesives, achieving efficient utilization of wood resources. This is why it is known as the "best value champion among engineered wood products." In China, particleboard is one of the most widely used substrates for melamine-faced panels (commonly known as "eco-boards" or "lacquer-free boards").
The fundamental difference between particleboard and MDF, plywood, and OSB lies in its structural particles (which retain a certain size and shape, rather than being ground into fibers or cut into veneers), giving it unique advantages in nail-holding capacity, sound insulation, and cost, though its surface smoothness and edge density are relatively inferior.
II. Classification System of Particleboard
2.1 By Manufacturing Process (Key Classification Dimension)
The production processes for particleboard mainly include flat-pressing, roll-pressing, and extrusion methods. Different processes determine the product structure and application directions:
| Process Type | Structural Characteristics | Density Range (g/cm³) | Key Process Points | Main Applications |
|---|---|---|---|---|
| Flat-Pressing (Multi-layer/Single-layer) | Three-layer structure (fine surface layer + coarse core layer) or gradient structure (particle size gradually changes from surface to core) | 0.5-0.85 | Graded particle layering — fine particles on top/bottom surfaces, coarse particles in core layer, formed by flat hot pressing | Furniture manufacturing (mainstream), architectural decoration, packaging |
| Roll-Pressing | Unidirectional continuous forming (non-oriented, but with slight directionality) | 0.4-0.7 | Particles are pressed between rotating rollers and endless steel belts; single particle orientation | Door core panels, packaging materials, low-density boards |
| Extrusion | Tubular structure (with longitudinally贯穿 tubular channels) | 0.35-0.55 | Particles extruded laterally in a die, creating "tubular structure" (similar to honeycomb but with longitudinal holes) | Hollow door core panels, partition walls, acoustic panels |
Advantages of Flat-Pressing Three-Layer Structure:
Surface fine particles provide smooth, flat surfaces (suitable for melamine laminating and paint finishing)
Core coarse particles provide good mechanical strength (bending and compression resistance) and excellent nail-holding capacity
Gradient density design from surface to core achieves a balance between performance and cost
2.2 By Raw Material
| Type | Raw Material Composition | Characteristics | Primary Producing Regions / Applications |
|---|---|---|---|
| Wood Particleboard | Wood particles (pine, poplar, eucalyptus, birch, etc.) | High strength, light color, good bonding performance | Global mainstream product |
| Bagasse Particleboard | Sugarcane bagasse (fiber residue after sugar extraction) | Low cost, renewable raw material, slightly lower density | Tropical sugar-producing regions (Brazil, India, Southern China) |
| Hemp/Flax Straw Particleboard | Industrial hemp or flax stalks | Excellent strength, lightweight, strong eco-friendly concept | Europe, North America |
| Straw Particleboard | Wheat straw, rice straw | Abundant raw material, eco-friendly, but short fibers result in slightly lower strength | Northern China, North America |
2.3 By Environmental Grade
The environmental grade of particleboard is determined by the type of adhesive used:
| Environmental Grade | Formaldehyde Emission (Chamber Method, mg/m³) | Common Adhesive Type | Applications |
|---|---|---|---|
| E1 | ≤0.050 (GB 18580-2025 mandatory) | Urea-formaldehyde (UF) + moderate melamine modification | General furniture, packaging |
| E0 | ≤0.025 | Melamine-modified urea-formaldehyde (MUF) | Mid-to-high-end furniture, interior decoration |
| ENF | ≤0.015 | MUF + formaldehyde scavenger / MDI (isocyanate) formaldehyde-free adhesive | Children's furniture, bedrooms, hospitals |
| HENF (Zero Formaldehyde Added) | ≤0.015 (with benzene, TVOC, etc. also compliant) | MDI formaldehyde-free adhesive | High-end residential, whole-house customization |
JINDIWOOD particleboard adopts MUF adhesive + formaldehyde scavenger dual technology. Standard products stably achieve E0, with custom options up to ENF.
2.4 By Surface Treatment Status
| Type | Characteristics | Main Applications |
|---|---|---|
| Raw Board (Unfinished) | Retains original particleboard surface, light yellow to light brown | Industrial use, packaging, internal structural components |
| Sanded Board | Surface sanded, smooth and flat | Paint substrate, laminating substrate |
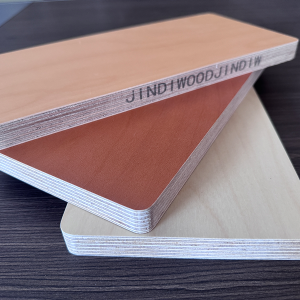
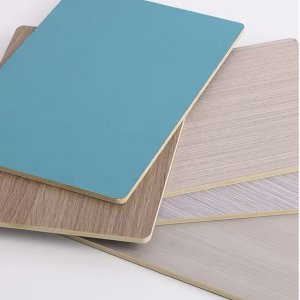
| Melamine-Faced Board | Surface laminated with melamine-impregnated paper (the most representative deep-processed particleboard product) | Panel furniture, cabinets, office furniture — the most common "lacquer-free board / eco-board" in the market |
| PVC-Faced Board | Surface laminated with PVC decorative film | Economy furniture, decoration |
| Wood Veneer-Faced Board | Surface bonded with natural wood veneer | High-end furniture, interior decoration |
III. Raw Material System of Particleboard
3.1 Wood Raw Materials
Particleboard has much lower raw material requirements than plywood and MDF. It can use:
Wood processing residues: sawdust, shavings, offcuts
Forestry residues: branchwood, tops, small-diameter logs (≤100mm)
Fast-growing plantations: poplar, eucalyptus, pine, etc. (5-8 year rotation)
Non-wood plant fibers: bagasse, hemp straw, crop straw, etc.
Comparison of Particle Morphology by Raw Material Species:
| Species | Particle Morphology | Density Contribution | Panel Color | Main Applications |
|---|---|---|---|---|
| Poplar | Soft, easily broken, moderate particle length (10-30mm) | Medium | White to cream | General-purpose furniture-grade particleboard |
| Pine | Contains natural resin, good particle toughness (20-40mm) | Higher (resin increases density) | Light yellow to light brown | Load-bearing furniture, packaging boards |
| Eucalyptus | Dense, high strength, harder particles (15-25mm) | High | Light reddish-brown | High-load furniture, flooring substrate |
| Mixed Hardwoods | Diverse particle morphology, varying lengths | Medium | Medium, may be uneven in color | Economy general-purpose boards |
3.2 Adhesive Systems — The Core of Particleboard
The adhesive content in particleboard is typically 8-15% of the oven-dry particle weight, similar to MDF (8-14%), slightly lower than plywood (based on veneer surface area) but higher than OSB (3-6%). Therefore, environmental control in particleboard is particularly critical.
| Adhesive Type | Application in Particleboard | Characteristics | Cost | Environmental Grade |
|---|---|---|---|---|
| Urea-Formaldehyde (UF) | Mainstream choice (accounts for >80%) | Fast curing, moderate bonding strength, lowest cost, but poor water resistance | Low | E1 |
| Melamine-Modified UF (MUF) | Mid-to-high-end products | Fast curing, better water resistance than UF, lower formaldehyde emission, moderate cost | Medium | E0/ENF |
| Isocyanate (MDI) | Premium formaldehyde-free products | Formaldehyde-free, excellent water resistance, high strength, but high cost (3-5x UF), moisture-sensitive | High | ENF/HENF |
| MUF + Formaldehyde Scavenger | Eco-friendly products | Reduces formaldehyde emission without changing core equipment | Medium | E0 |
Principle of Formaldehyde Scavenger:
Reactive nitrogen-containing compounds (such as urea, melamine, amides) are added to UF resin or sprayed separately onto particle surfaces. During hot pressing and in-service use, these substances react with free formaldehyde to form stable hydroxymethyl derivatives (irreversible reaction), effectively "chemically locking" formaldehyde inside the board, preventing its release into the air.
3.3 Auxiliary Additives
| Additive | Addition Rate (% of Oven-Dry Particle Weight) | Function |
| :--- | :--- | :--- | :--- |
| Paraffin Emulsion (Water Repellent) | 0.8-2.0% | Reduces thickness swelling from water absorption, improves moisture resistance |
| Hardener (Ammonium Chloride / Ammonium Sulfate) | 0.5-2.0% (relative to adhesive solids) | Accelerates UF/MUF curing reaction, shortens hot pressing time, improves production efficiency (typically reduces hot press cycle by 20-30%) |
| Coupling Agent (Silane-based, for MDI systems only) | 0.2-0.5% | Improves wetting and chemical reaction efficiency between MDI adhesive and wood particles |
IV. Particleboard Production Process Flow
4.1 Process Flowchart
Raw Material Receiving → Chipping → Particle Preparation → Wet Particle Storage → Drying → Screening (Surface/Core Separation)
  → Glue Application (Surface + Core, different formulations) → Mat Forming (Three-layer/Gradient) → Pre-Pressing → Hot Pressing
  → Cooling & Conditioning → Trimming & Sanding → Grading & Packaging → Finished Product
4.2 Technical Details of Each Process Step
Step 1: Particle Preparation
Raw materials are processed into wood chips (20-40mm length, 3-5mm thickness) through a chipper, then further pulverized into particles by a hammer mill or ring flaker. The geometric dimensions of the particles are key parameters determining the physical and mechanical properties of particleboard:
| Particle Type | Length (mm) | Width (mm) | Thickness (mm) | Length/Thickness Ratio |
|---|---|---|---|---|
| Surface Fine Particles | 5-15 | 0.5-3 | 0.15-0.3 | 20-60 |
| Core Coarse Particles | 15-35 | 3-8 | 0.3-0.6 | 50-100 |
Mechanical Effects of Particle Morphology:
Longer particles and higher length/thickness ratios → higher bending strength and modulus of elasticity (long particles act as reinforcement phase within the board, similar to rebar in concrete)
Wider particles → better nail-holding capacity (wider particles provide more bonding surface area, and nails must pull the particles out of the matrix when withdrawn, dissipating more energy)
Smoother particle surfaces → better adhesive wetting and higher bonding strength (angular or rough surfaces reduce contact area, hindering bonding)
Particle Size Distribution Requirements (Standard): Particles passing through a 6-mesh screen (3.35mm) ≤5%; fine powder passing through a 60-mesh screen (0.25mm) ≤8%. Size qualification rate directly affects glue application uniformity and panel performance.
Step 2: Particle Drying
Wet particles (moisture content 30-60%) are dried in single-pass or triple-pass rotary drum dryers to the target moisture content.
Heat Source: Hot air furnace (combusting biomass fuel — bark, sanding dust, waste particles)
Hot Air Temperature: 160-220°C (inlet), 80-100°C (outlet)
Target Moisture Content after Drying: 2-5% (before entering the glue applicator)
Precise Control of Drying Temperature:
Excessively high temperature (>230°C) → particle surface carbonization ("over-burning"), reduced particle strength, darker color, and extremely poor adhesive wetting on carbonized surfaces (leading to significant bonding strength reduction)
Excessively low temperature (<140°C) → high moisture content (>8%), adhesive dilution during application, and moisture vaporization during hot pressing causing blistering
Particle residence time in the dryer is typically 3-8 minutes.
Step 3: Screening
Dried particles are screened through mechanical vibrating screens:
Fine particles (passing through 6-10 mesh screens) → sent to surface layer bins (for top and bottom surface layering)
Coarse particles (retained on 6-10 mesh screens) → sent to core layer bins (for middle layer layering)
The separation of fine and coarse particles is a prerequisite for achieving the three-layer structure (fine-coarse-fine). Some production lines use air classifiers instead of mechanical screens for higher efficiency and less damage to particle morphology.
Step 4: Glue Application
Surface and core particles enter high-speed mixing glue applicators (blenders) separately. Adhesive is sprayed in by high-pressure atomization (nozzle pressure 2-4 MPa), simultaneously injecting hardener solution and paraffin emulsion.
Differences in Glue Application Rates Between Surface and Core Layers:
| Parameter | Surface Particles | Core Particles | Reason |
|---|---|---|---|
| Glue Application Rate (% of OD particle weight) | 10-14% | 8-12% | Surface fine particles have higher specific surface area than core coarse particles, requiring more adhesive to ensure surface strength, density, and decorative layer bond |
| Hardener Addition Rate (% of adhesive solids) | 0.5-1.5% | 1.0-2.0% | Core layer has slower heat transfer; higher hardener concentration compensates for slower temperature rise ("thermal lag effect") to ensure complete core curing within the same press cycle |
| Paraffin Addition Rate (% of OD particle weight) | 0.5-1.0% | 1.0-1.5% | Core coarse particles have more capillary structures (micropores) allowing easier moisture penetration; higher paraffin content seals these channels to reduce water absorption |
Particle Moisture Content After Glue Application: Rises from 2-5% to 8-12% due to moisture from adhesive and hardener solutions, creating conditions for subsequent hot pressing (moderate moisture generates steam during pressing, aiding heat transfer to the core; excessive moisture causes blistering).
Step 5: Mat Forming
Glue-applied surface and core particles are separately formed into a continuous mat using mechanical (or air-flow) formers.
Three-Layer Mat Forming Process:
Bottom layer (lower surface): Surface fine particles, thickness approx. 1.5-3mm
Core layer: Core coarse particles, thickness approx. 70-80% of total mat thickness (for panels ≥12mm thick, the core is the main body)
Top layer (upper surface): Surface fine particles, same thickness as bottom layer
The formed mat thickness is approximately 2.5-3.5 times the final panel thickness (expansion ratio controlled by hot pressing pressure and temperature).
Step 6: Pre-Pressing and Hot Pressing
Pre-Pressing: The mat is pre-pressed at 0.5-1.0 MPa, compressing the mat thickness by 30-50%, improving mat strength and thermal conductivity for transfer into the hot press.
Hot Pressing: The mat enters a multi-opening hot press (typically 12-20 openings, primarily for medium-density/thick panels) or a continuous flat-press (CPS, for mass production of thin and general-purpose particleboard).
| Hot Pressing Parameter | Typical Value | Effect on Particleboard Quality |
| :--- | :--- | :--- | :--- |
| Hot Pressing Temperature | 180-210°C | Too high → particle surface carbonization (dark surface color), adhesive aging and embrittlement; too low → insufficient adhesive curing ("under-cured core"), panel spring-back |
| Unit Pressure | 1.5-3.5 MPa (depending on density grade) | Too high → particle crushing, excessive density, wasted fiber resources; too low → insufficient mat densification, loose panel, low strength |
| Hot Pressing Time | 0.5-0.9 min/mm (e.g., 9-16 min for 18mm board) | Too short → incomplete core curing; too long → low production efficiency, particle thermal degradation (embrittlement) |
Physical and Chemical Changes Within the Mat During Hot Pressing:
The mat surface reaches target temperature (180-210°C) within 15-30 seconds; adhesive begins cross-linking and curing
The core temperature reaches ≥150°C (UF/MUF curing temperature window) within 3-6 minutes; adhesive completes curing
Steam pressure from moisture vaporization accumulates in the core; if not released in time, it causes "blistering" or "delamination" after the board exits the press — therefore, slow pressure release (stage-wise pressure reduction) is required in the final stage of hot pressing to allow controlled steam escape
Step 7: Cooling, Conditioning, Trimming, and Sanding
Cooling: Boards exiting the hot press are at 80-120°C; they are cooled to room temperature (≤40°C) via a board cooling line to prevent deformation or sticking during stacking.
Conditioning (Moisture Balance): Cooled boards are stored in the warehouse for 48-72 hours to allow internal temperature and moisture content to equilibrate with the environment and release residual stress.
Trimming: Rough boards are cut to standard dimensions (1220×2440mm) on a trimming saw, removing loose edges (typically 25-50mm per side).
Sanding: Board surfaces are sanded on wide-belt sanders (rough sanding 60-100 grit + fine sanding 150-240 grit), with sanding allowance 0.3-0.8mm (both sides combined), achieving thickness precision of ±0.2mm and surface roughness Ra≤3.2μm.
Step 8: Grading and Packaging
After visual grading, boards are strapped with packing bands (typically 20-50 sheets per package), covered with PE protective film, and labeled with product specifications, environmental grade, and batch number.
V. Core Technical Specifications of Particleboard
5.1 Physical and Mechanical Performance Requirements (GB/T 4897-2015)
Particleboard performance is classified into types from P1 (non-load-bearing boards in dry conditions) to P7 (load-bearing boards / wet conditions). Below are the technical requirements for the commonly used P2 type (load-bearing boards in dry conditions) for furniture manufacturing:
| Performance Indicator | Unit | National Standard (P2) | JINDIWOOD Standard |
|---|---|---|---|
| Density | g/cm³ | 0.50-0.85 | 0.65-0.75 (18mm board) |
| Modulus of Rupture (MOR) | MPa | ≥13 (long.) / ≥11 (trans.) | ≥16 |
| Modulus of Elasticity (MOE) | MPa | ≥1600 (long.) / ≥1400 (trans.) | ≥2200 |
| Internal Bond Strength (IB) | MPa | ≥0.40 | ≥0.55 |
| Surface Bond Strength | MPa | ≥0.80 | ≥1.0 |
| Thickness Swelling (24h) | % | ≤15 (P2) / ≤8 (P5 moisture-resistant) | ≤12 |
| Moisture Content | % | 5-11 | 6-9 |
Effect of Density on Particleboard Performance:
Too low density (<0.55 g/cm³): insufficient strength, poor nail-holding capacity, loose surface, prone to "powder shedding" after sanding
Too high density (>0.85 g/cm³): heavy weight, severe tool wear (increased costs), higher material costs
Non-uniform density (surface-core density difference ≥0.15 g/cm³): board warping, "soft and hard spots" after sanding (different cutting depths on areas of different densities causing localized depressions or protrusions)
5.2 Nail-Holding Capacity
Particleboard's nail-holding capacity exceeds MDF due to its core coarse particle structure, but is lower than plywood and OSB:
| Test Item | Particleboard (18mm, ρ=0.68g/cm³) | MDF (18mm, ρ=0.75g/cm³) |
|---|---|---|
| Face Nail-Holding (perpendicular, screw dia. 3.5mm, 15mm penetration) | 800-1100 N | 700-1000 N |
| Edge Nail-Holding (edge direction, same test conditions) | 500-800 N | 300-600 N |
Why Particleboard Outperforms MDF in Nail-Holding:
Core coarse particles provide "anchorage" action when screws are driven — the screw threads interact with wood fibers in the particles, resisting withdrawal not only through friction at the bonded interface but also through embedding into particle interiors
MDF has a homogeneous fiber structure; screw withdrawal relies primarily on shear failure at the bonded interface, lacking the additional anchorage points provided by particles
Engineering Methods to Improve Particleboard Nail-Holding:
Increase density (higher coarse particle proportion) → enhance the number and strength of anchorage points
Control pre-drilled hole diameter at 70-80% of screw diameter (e.g., 2.7-2.9mm drill for 3.5mm screws) to ensure effective thread engagement with particles
5.3 Formaldehyde Emission
Formaldehyde emission from particleboard is one of the most closely watched environmental indicators by consumers. Different grades show significant differences:
| Environmental Grade | Formaldehyde Emission (Chamber Method, mg/m³) | Adhesive Solution |
|---|---|---|
| E1 | ≤0.050 | Standard UF (U/F molar ratio 1:1.2-1.5) |
| E0 | ≤0.025 | MUF or UF + formaldehyde scavenger (e.g., melamine, urea) |
| ENF | ≤0.015 | High-proportion MUF (melamine substitution ≥30%) + efficient formaldehyde scavenger, or MDI |
| HENF | ≤0.015 (all parameters compliant) | Pure MDI formaldehyde-free adhesive |
Technical Approaches to Reduce Formaldehyde Emission:
Lower UF resin F/U molar ratio: Reduce from conventional 1.3-1.5 to 1.0-1.1, significantly reducing free formaldehyde (but may slightly reduce bonding strength, compensated by process optimization)
Add formaldehyde scavengers: Introduce scavengers (e.g., melamine, urea, amides) during glue application or after hot pressing to react with and consume free formaldehyde
Adopt MUF or MDI adhesives: Fundamentally reduce or eliminate the source of free formaldehyde
5.4 Thickness Swelling from Water Absorption (Moisture Resistance)
Moisture resistance is a relatively weaker aspect of particleboard. Thickness swelling (TS) directly affects service life in humid environments:
| Grade | 24h Thickness Swelling (%) | Suitable Environment |
|---|---|---|
| P2 (Standard) | ≤15 | Indoor dry conditions (annual avg. 20°C, RH ≤65%) |
| P5 (Moisture-Resistant) | ≤8 | Indoor humid conditions (RH 65-85%, occasional condensation) |
| P7 (Exterior) | ≤5 | Semi-outdoor / high-humidity high-load environments (special formulation required) |
Technical Methods to Reduce Thickness Swelling:
Increase paraffin water repellent addition rate (from 1.0% to 1.5-2.0%)
Increase hot pressing temperature (enhances plastic flow, reduces capillary channels)
Use MUF adhesive (MUF has better water resistance than UF)
Use MDI adhesive (cured polyurethane cross-linking network blocks water molecule penetration)
VI. Surface Treatment and Laminating Technologies for Particleboard
Raw particleboard surfaces are relatively rough, and particle particles are visible on the edges ("edge particle exposure"). Therefore, the vast majority of particleboard requires surface finishing before use in end products.
6.1 Melamine-Impregnated Paper Laminating (Most Common Method)
Melamine-impregnated paper is directly pressed onto the particleboard surface at high temperature (180-210°C) and high pressure (2.5-3.5 MPa) in a single-step process.
Characteristics:
Achieves decorative effect and wear resistance in one operation (paper contains melamine resin and wear-resistant α-Al₂O₃)
High surface hardness (pencil hardness ≥3H), scratch-resistant, heat-resistant, stain-resistant
The most mainstream laminating method in panel furniture, cabinet, and wardrobe door manufacturing — the typical process for "eco-boards" / "lacquer-free boards"
JINDIWOOD melamine-faced particleboard adopts this process, with a full range of designs and support for synchronized embossing (pattern-matched texture) customization.
6.2 Wood Veneer Laminating
Natural wood veneer (thickness 0.3-0.6mm) is bonded to the particleboard surface by hot or cold pressing. Suitable for high-end furniture and interior decoration. Wood-veneered particleboard edges require fine edge-banding (using matching color veneer edge tape or solid wood edge banding) to conceal edge particle exposure.
6.3 Paint Finishing
Sanded particleboard can be paint-finished (PU, UV, water-based paints, etc.), but requires a sealing primer first (to seal capillaries and micropores, preventing topcoat over-absorption causing "sink-in" or "pinholes"), followed by sanding and topcoat application. Paint finishing costs are higher than MDF (due to particleboard's greater surface porosity), primarily used in cost-sensitive applications with certain environmental and decorative requirements (e.g., office furniture panels, commercial display cabinets).
6.4 Direct Use (Raw Board Applications)
Raw particleboard is primarily used for:
Industrial uses such as packaging boxes and pallets
Building partitions and ceilings (requiring additional finishing)
Speaker enclosures (internal partitions or non-visible components)
Furniture internal structural components (cabinet back panels, drawer bottoms, etc.)
VII. Application Scenarios of Particleboard
7.1 Furniture Manufacturing (Largest Application, ~70%)
| Furniture Type | Application Areas | Recommended Grade | Selection Rationale |
|---|---|---|---|
| Custom Panel Furniture | Wardrobe carcasses, bookcase shelves, TV cabinets | E0/ENF melamine-faced | Rich designs, compliant environmental standards, high processing efficiency |
| Office Furniture | Desktops, filing cabinets, conference tables | E0 melamine-faced | Wear-resistant, stain-resistant, easy to clean, cost-effective |
| Cabinets | Carcasses (P5 moisture-resistant), door core materials | P5 moisture-resistant (E0) | Good moisture resistance, dimensional stability |
| Kitchen Furniture | Sink cabinets (require special waterproofing) | P5 moisture-resistant or MDI ENF + sealed edges | Moisture resistance is critical |
| Children's Furniture | Bed boards, desks, wardrobes | ENF (MDI or high-MUF + scavenger) | Zero formaldehyde, health and safety |
| Public Furniture | Library shelving, hospital seating | P2 (E0, optional fire-retardant treatment) | Balanced properties, controllable cost |
7.2 Architectural Decoration
Partition walls / interior wall panels: P2 particleboard (12-18mm), used as substrate for partition walls, covered with gypsum board or decorative panels
Ceilings: Lightweight particleboard (8-12mm), for ceiling substrates (requires fire-retardant treatment)
Floor underlayment (leveling layer): High-density particleboard (20-25mm), as leveling material beneath wood flooring, providing flat substrate and sound insulation
7.3 Packaging and Industrial Applications
| Application | Recommended Specifications | Function | Selection Rationale |
|---|---|---|---|
| Heavy-Duty Packaging Crates | 15-18mm, P2 | Protects machinery, electronics | Reliable strength, far lower cost than solid wood, fumigation-free for export |
| Logistics Pallets / Dunnage | 12-18mm, P2 (moisture-treated) | Load support during storage/transport, forklift operations | Replaces solid wood pallets, 30-50% cost reduction, no quarantine risks |
| Speaker Enclosures | 12-18mm, high-density | Speaker mounting substrate, enclosure structure | Moderate density, good damping (sound absorption better than MDF, lower coloration), low cost |
VIII. Comparison of Particleboard with Other Panel Materials
| Comparison Dimension | Particleboard (P2) | MDF (Standard) | Plywood (Furniture) | OSB (OSB/2) |
|---|---|---|---|---|
| Raw Material Utilization Rate | 85-90% (extremely high) | 70-75% (high) | 40-50% (low) | 80-85% (high) |
| Density (g/cm³) | 0.65-0.75 | 0.70-0.85 | 0.50-0.70 | 0.60-0.70 |
| MOR (MPa) | 13-16 (P2) / 20-25 (high-strength) | 20-25 | 40-70 | 22-28 |
| Internal Bond Strength (MPa) | ≥0.40 | ≥0.55 | ≥0.70 | ≥0.40 |
| Surface Smoothness | Good (but inferior to MDF) | Excellent | Good | Fair |
| Edge Sealing Requirement | Required (particle exposure) | Required (fiber exposure, moisture absorption) | Recommended (but not mandatory) | Recommended (edge strength relatively better) |
| Face Nail-Holding (N) | 800-1100 | 700-1000 | 1500-2500 | 1200-1600 |
| Moisture Resistance | Moderate (P5 for improved) | Poor (high swelling) | Excellent (waterproof adhesive available) | Good (OSB/2 meets P2; OSB/3/4 moisture-resistant) |
| Environmental Grade Potential | E1/E0/ENF | E1/E0/ENF | E1/E0 | ENF (MDI) |
| Cost | Lowest | Low | High | Medium-High |
| Processability | Good (sawing, drilling, edge-banding) | Excellent (carving, profiling, milling) | Good (sawing, planing, nailing) | Good (similar to solid wood) |
| Typical Applications | Panel furniture, cabinets, office furniture | Decorative panel substrate, carved parts, door panels | Construction formwork, high-end furniture, marine | Building structures, load-bearing furniture |
IX. Common Quality Misconceptions and Facts
Misconception 1: "All particleboard is low-end."
Fact: Particleboard is the world's largest-volume, most widely used, and most technologically mature engineered wood product. It is used everywhere from inexpensive furniture costing tens of yuan to premium custom cabinetry costing tens of thousands. The performance gap between high-end and low-end particleboard is enormous —
High-end particleboard features more uniform density (surface-core density difference ≤0.10g/cm³), higher internal bond strength (≥0.55MPa), stronger nail-holding capacity (≥1000N), better moisture resistance (TS≤8%), and achieves E0/ENF environmental grades.
Low-end particleboard suffers from non-uniform density, insufficient strength, and higher risk of exceeding environmental limits.
Therefore, "it's certain low-quality particleboards that are low-end, not the particleboard category itself." Choosing the right particleboard grade and supplier is more important than simply rejecting the category.
Misconception 2: "Particleboard has high formaldehyde — it's not eco-friendly."
Fact: The environmental grade of particleboard is entirely determined by the adhesive used, not by the category name "particleboard." E0 and ENF particleboards are already widely available.
MUF + efficient formaldehyde scavenger → E0 (≤0.025mg/m³)
MDI formaldehyde-free adhesive → ENF (≤0.015mg/m³), truly "zero formaldehyde added"
When purchasing, look for test reports, environmental grade labels (E0/ENF), and brand reputation — this is far wiser than avoiding "particleboard."
Misconception 3: "Particleboard is inferior to solid wood."
Fact: Particleboard and solid wood are materials of different dimensions; there is no simple "which is better" — it depends on the application.
Stability: Particleboard has low anisotropy (longitudinal/transverse strength ratio ~1.0-1.2), deforming far less than solid wood under temperature/humidity changes (coefficient of thermal expansion about 1/3 to 1/2 of solid wood)
Strength: High-quality particleboard (high-density) has bending strength (≥20MPa) reaching 2-3 times that of some low-density solid woods (e.g., paulownia, balsa)
Nail-holding: Particleboard's edge nail-holding is inferior to solid wood (solid wood in the parallel-to-grain direction has extremely high nail-holding), but face nail-holding is comparable to some softwoods
Eco-friendliness/Cost: Particleboard can achieve zero formaldehyde at prices far below solid wood
Conclusion: Particleboard outperforms solid wood in stability, cost-effectiveness, and controllable environmental performance; solid wood outperforms particleboard in nail-holding (parallel-to-grain), natural texture, and durability (creep resistance under long-term loading). Both have their appropriate applications — choose based on specific requirements.
Misconception 4: "Particleboard can't bear weight."
Fact: This entirely depends on particleboard grade and thickness.
Standard P2 particleboard (density 0.65-0.70g/cm³, 18mm thickness): Under 600mm span, 200kg/m² load, deflection is approx. 1.8-2.2mm — fully meeting daily load requirements for bookshelves, desktops, etc. (shelf deflection limit is typically L/250 ≈ 2.4mm; MDF under same conditions deflects approx. 1.8-2.0mm)
High-density particleboard (≥0.80g/cm³, 25mm thickness): MOR up to 25-30MPa, suitable for heavy-duty applications like library shelving and warehouse racking
Multiple layers or additional support structures (cross-bracing, reduced span) can further enhance load capacity
Misconception 5: "Particleboard has poor moisture resistance."
Fact: This is typically based on a stereotype of low-end UF-glued particleboard (cheap boards).
P5 moisture-resistant particleboard (MUF adhesive, paraffin addition ≥1.5%): 24h TS ≤8%, suitable for kitchens, bathroom dry areas, and other humid environments — but not for long-term water immersion
MDI particleboard: MDI adhesive itself has excellent hydrolysis resistance; combined with paraffin water repellent, 24h TS can be reduced to ≤6-7%, approaching P7 (exterior) levels
For extremely high moisture protection requirements (e.g., long-term high-humidity environments, basements), use P5 or MDI particleboard with enhanced edge sealing (using PUR hot-melt adhesive for waterproof edge-banding)
X. Future Technology Trends of Particleboard
10.1 High Performance and Lightweighting
High-strength particleboard: Optimizing particle morphology (oriented particles with aspect ratio ≥100), using MDI adhesive, and optimizing hot pressing processes to increase MOR to ≥25MPa (approaching MDF), partially replacing OSB in dry applications.
Lightweight high-strength particleboard: Using foaming technology or gradient density structures (high-density surface, low-density core) to maintain sufficient mechanical strength (MOR ≥12MPa) at densities ≤0.55g/cm³, reducing furniture weight and raw material consumption.
Ultra-thin particleboard: Developing thin particleboard ≤6mm for non-load-bearing applications such as furniture back panels, drawer bottoms, and packaging dividers, replacing MDF at lower cost.
10.2 Environmental Protection and Formaldehyde-Free Technology
Low F/U molar ratio UF adhesive adoption: UF adhesives with F/U ratios reduced from 1.3 to 1.0-1.1 have been industrialized. Combined with advanced formaldehyde scavengers, E0 has become the standard, with ENF moving toward widespread adoption.
Bio-based adhesive applications: Lignin-based adhesives (paper industry by-product, cost close to UF) and tannin-based adhesives (bark extract, suitable for exterior grades) are gradually being industrialized, with potential to partially replace petroleum-based adhesives.
Formaldehyde-free particleboard (MDI) rapid growth: MDI-bonded particleboard is expected to account for over 20% of China's total particleboard production by 2028 (approx. 8% in 2025), with costs declining as domestic MDI production capacity expands.
10.3 Moisture Resistance and Functionalization
Hydrophobic particleboard: Surface modification of particles using nano-hydrophobic agents (e.g., silanes) rather than relying solely on paraffin water repellents, reducing 24h TS to ≤4-5%, approaching plywood's waterproof performance.
Fire-retardant particleboard: Adding phosphorus-nitrogen halogen-free flame retardants (in adhesive or sprayed as separate additive) to achieve B1 grade (difficult to ignite), meeting requirements for public buildings and commercial spaces.
Antibacterial/mold-resistant particleboard: Adding silver ions or organic antibacterial agents (e.g., Zinc Pyrithione (ZPT)) to surface particles, achieving ≥99% antibacterial rate, suitable for hospitals, schools, and food-related applications.
10.4 Smart Manufacturing
In-line quality monitoring systems: Using Near-Infrared (NIR) spectroscopy for on-line detection of particle moisture content and glue application rate (error ≤±0.3%), and X-ray densitometers for online density profiling (resolution ≤±2mm), achieving 100% quality traceability across all batches with real-time process parameter adjustment.
AI visual defect detection: Machine vision systems based on deep learning algorithms (Convolutional Neural Networks) for automatic defect recognition and grading on panel surfaces (scratches, indentations, glue spots, etc.) with accuracy ≥95% and efficiency 10-20 times human inspection, replacing manual visual inspection.
MES/ERP system integration: Fully integrating order, formulation, production, quality, warehousing, and logistics data to achieve digital closed-loop management from order to delivery.

JINDIWOOD · Engineered for Certainty — Every particle recombined builds a foundation of certainty for the stability of furniture and the health of living spaces.
This article is an original technical publication by JINDIWOOD. Reproduction must indicate the source.