中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
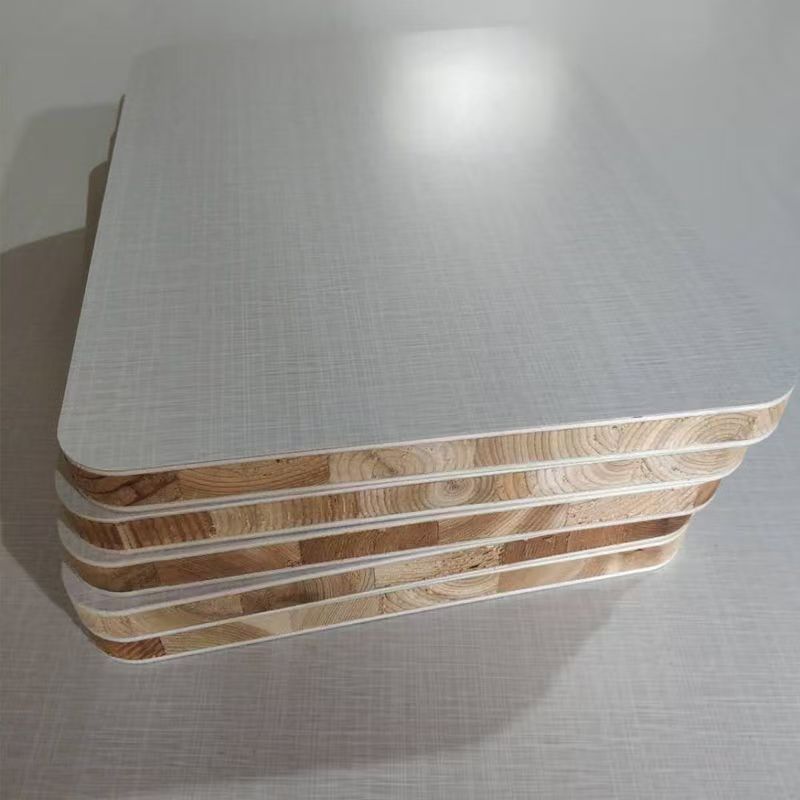
I. Basic Concept of Glued Laminated Timber
Glued Laminated Timber (abbreviated as Glulam), also known as finger-jointed board, finger-jointed timber, or laminated solid wood panel, is one of the three major engineered wood products, alongside Wood I-joists and Laminated Veneer Lumber (LVL).
Glulam is manufactured by taking narrow, short solid wood strips, removing natural defects such as knots, decay, and cracks, then joining them longitudinally using adhesives (typically through finger joints, similar to interlocking fingers), followed by lateral edge-gluing to increase width, and finally sanding both surfaces. Through industrial processing, it transforms short and small pieces of solid wood (which would otherwise be unusable) into engineered materials meeting specific dimensional and shape requirements, achieving the principle of "utilizing small and inferior timber for superior applications."
Core Essence: Glulam is an "industrial recombination of natural solid wood." It retains all the aesthetic and processing advantages of natural wood — grain, color, texture, and workability — while eliminating common natural defects such as knots, cracks, warping, and twisting through "defect removal + finger jointing + edge-gluing recombination." This results in material strength, stability, and dimensional capabilities that surpass the limits of natural logs.
Industry Status: According to the China National Forest Products Industry Association, China's annual production of glulam exceeded 15 million cubic meters in 2025, with non-structural glulam (furniture grade) accounting for over 70% and structural glulam (construction grade) accounting for approximately 30%. Glulam has been used in Japan, Europe, and North America for over half a century, and in China, it has developed rapidly with the rise of custom furniture and timber construction.
JINDIWOOD Glulam Product Range:
Non-Structural Glulam (Furniture Grade): Uses eco-friendly adhesives (MUF/MDI), achieving environmental grades from E0 to ENF. Widely used in high-end furniture, cabinets, wooden doors, staircases, etc.
Structural Glulam (Construction Grade): Uses high-performance adhesives (PRF/MDI), meeting load-bearing structural requirements. Used in long-span timber beams, gymnasiums, bridges, and other engineering projects.
II. Manufacturing Raw Material System
2.1 Log Selection — From "Natural Defects" to "Industrial Raw Material"
Glulam has significantly higher raw material tolerance than solid sawn timber. It can fully utilize small-diameter logs, curved timber, branchwood from natural and plantation forests, as well as low-quality logs that would otherwise be discarded due to knots, cracks, and color variations in traditional solid wood processing.
| Raw Material Type | Source | Advantages in Glulam | Typical Species |
|---|---|---|---|
| Small-diameter logs (≤200mm) | Plantation thinning, secondary forest improvement | Cannot be sawn into long pieces (>2m), but can be finger-jointed to produce large-size panels | Poplar, Pine, Fir |
| Curved/defective logs | Natural forest or plantation harvest residues | Traditional sawn timber requires cutting out curved sections; glulam can recombine curved portions through finger jointing, improving yield to 75-85% (far higher than 40-50% for traditional sawn timber) | Oak, Walnut, Beech |
| Fast-growing plantations (rotation 8-15 years) | Large-scale planted forests | Soft texture, low density (approx. 0.35-0.50g/cm³), wide growth rings, insufficient natural strength — significantly improved through finger jointing and lamination, used in non-load-bearing furniture | Poplar, Eucalyptus, Pine |
Species Selection and Application Range:
| Species | Density (g/cm³, air-dried) | Material Characteristics | Applications |
|---|---|---|---|
| Pine | 0.40-0.55 | Straight grain, moderate resin content, excellent bonding properties, light yellow color | Structural glulam (beams/columns), furniture frames, interior decoration |
| Poplar | 0.35-0.45 | Light and soft, light color, easy to dry and process, but lower strength | Non-structural glulam (furniture components, door core panels, picture frames) |
| Beech | 0.65-0.75 | Dense and hard, fine texture, extremely high bonding strength, warm color | High-end furniture, cabinets, stair treads, high-strength structural beams |
| Oak | 0.65-0.85 | Extremely high hardness, attractive coarse grain, good decay resistance, high bonding requirements (due to tannic acid content) | High-end furniture, flooring, architectural decoration, structural/decorative dual use |
| Walnut | 0.55-0.65 | Elegant color (dark brown), attractive grain, dimensional stability | Premium furniture, musical instruments, interior decoration |
| Fir | 0.35-0.45 | Light and soft, straight grain, easy to process, good preservative treatment | Structural glulam (light-frame construction), packaging materials |
2.2 Moisture Content Control — The Core of Glulam Stability
The reason glulam offers superior dimensional stability compared to natural solid wood lies in precise moisture content control during production and the elimination of internal stress through finger jointing:
Raw Material Drying: Glulam production requires drying logs or sawn timber to 6-12% (final equilibrium moisture content), far more stringent than the 12-15% typical for ordinary solid wood furniture.
Drying Process: Uses low-temperature/conventional kiln drying (gradual temperature increase from 40-70°C) rather than high-temperature kiln drying, avoiding micro-cracks ("surface hardening") on the wood surface. This takes 30-50% longer than traditional drying.
Conditioning (Acclimatization): Before finger jointing and edge-gluing, each piece must be stored for 5-7 days under constant temperature and humidity conditions (temperature 20±2°C, relative humidity 65±5%) to ensure moisture content variation between pieces is ≤±1.5%. This step is critical — if moisture content is inconsistent, the reassembled panel will develop internal stresses (differential shrinkage/swelling) in different directions during use, leading to warping or cracking.
Effect of Moisture Content on Glulam Performance:
| Moisture Content State | Effect |
|---|---|
| Too dry (<6%) | Increased wood brittleness, reduced finger joint strength, tendency to chip during processing, excessive adhesive absorption ("dry glue"), reduced bond strength |
| Optimal (6-12%) | Optimal processing and bonding state, dimensionally stable, optimal mechanical properties |
| Too wet (>12%) | Moisture vaporization during bonding creates bubbles ("foaming glue line"), reduced finger joint strength, shrinkage and cracking of finished product in dry environments, extremely high deformation risk |
III. Core Processes of Glulam — Finger Jointing and Edge Gluing
3.1 Finger Jointing Technology — From Short Pieces to Long Stock
Finger jointing is the key core technology in glulam production. Its essence involves machining the ends of multiple short pieces (typically 0.3-1.2m in length) into toothed profiles, applying adhesive, and pressing them together longitudinally to form continuous stock of any length.
Design Principles of Finger Joint Geometry:
Finger joints are created by milling a series of toothed protrusions and recesses at the ends of wood pieces (similar to interlocking fingers). After adhesive application and pressing, the joint relies on mechanical interlocking + adhesive curing to achieve longitudinal connection. The joint design must meet the following mechanical requirements:
| Joint Parameter | Typical Value (Furniture/Structural Grade) | Function & Impact |
|---|---|---|
| Finger Length (L) | 10-20mm (furniture) / 20-40mm (structural) | Longer fingers provide larger bonding area and higher joint strength. Structural grade requires longer fingers for safety margins |
| Finger Width (B) | 3-6mm | Smaller width means more fingers (same length), larger bonding area, but requires higher machining precision |
| Finger Pitch (P) | 5-12mm | Affects "interlocking" density and adhesive distribution uniformity |
| Tip Clearance (Δ) | 0.1-0.3mm | Space reserved for adhesive. Too small → glue line too thin, insufficient strength; too large → glue line too thick, "glue seam" after curing shrinkage (affects appearance and water resistance) |
| Finger Angle (α) | 5-15° | Affects "wedging effect" under tension. Smaller angles provide stronger wedging but are more difficult to machine |
Mechanical Verification of Finger Joint Strength (EN 385 — European Standard for Structural Finger-Jointed Timber):
The failure mode in tensile tests of finger joints should show wood failure ≥75% (i.e., failure occurs primarily in the wood itself, not in the adhesive layer or tooth interface). If wood failure is too low (<50%), bonding quality is substandard, posing safety risks in structural applications.
Precision Control in Finger Jointing Operations:
End Trimming: Ends of each short piece are simultaneously sawn using a double-end tenoner (squaring), ensuring both ends are parallel and perpendicular to the length direction (perpendicularity deviation ≤0.2mm). Otherwise, the joined piece will be "bent" or "twisted."
Finger Joint Milling: Uses specialized finger joint cutter heads (profile tools) to mill the tooth profile. Milling speed: 6000-8000rpm, feed rate: 10-20m/min.
Adhesive Application: Adhesive is applied to the finger joint surfaces (typically by roller coating or spraying), with application rate controlled at 150-250g/m² (per finger surface area). Insufficient adhesive → inadequate bonding area, reduced joint strength; excessive adhesive → waste and glue-line appearance issues.
Longitudinal Pressing (Jointing): Pressing the adhesive-coated pieces together in a longitudinal press (end press) along the length direction. Pressing pressure is typically 5-15 MPa (adjusted for species and density), pressing time 1-5 seconds. Insufficient pressure → incomplete tooth engagement ("loose joint"); excessive pressure → crushed finger tips, wood fiber damage, strength reduction.
Curing and Conditioning: After pressing, the joined stock is placed in a controlled environment for 8-24 hours (depending on adhesive type and ambient temperature) to allow full curing of the adhesive. The stack must be kept flat to prevent bending.
Strength Evaluation of Joined Stock (Destructive Testing):
For every 1,000 finger-jointed pieces produced, 1 piece is randomly sampled for four-point bending test (EN 408) and tensile test (EN 1194) to ensure joint quality acceptance rate ≥99%. Acceptance criteria: failure load ≥90% of design requirement, with failure mode primarily "wood failure" (wood fracture) rather than "adhesive failure" (adhesive separation).
3.2 Edge Gluing Technology — From Narrow Pieces to Wide Panels
After finger jointing to achieve the required length, the pieces are joined side-by-side in the width direction (side-gluing) to form panels of the desired width.
| Edge Gluing Method | Process Characteristics | Applications | Appearance Effect |
|---|---|---|---|
| Butt Joint (adhesive/non-adhesive) | Adjacent strips are planed and directly assembled (some processes use minimal adhesive; others rely on subsequent sanding and compression) | High-end furniture requiring continuous, natural grain with minimal visible joints | Extremely fine joint lines visible (approx. 0.1-0.2mm), no glue lines, natural grain transition |
| Finger Joint Edge-Gluing (side finger joint) | Adjacent strips have toothed edges machined, adhesive applied, and laterally pressed | Structural or decorative applications requiring lateral strength (resistance to side forces) | Small toothed texture at joints, decorative effect |
| Adhesive Edge-Gluing | Adjacent strips are edge-coated with adhesive and laterally pressed (same principle as finger jointing) | Standard furniture-grade glulam — the mainstream method | Visible glue lines at joints (approx. 0.1-0.3mm, slightly darker than wood) |
Key Quality Control Points for Edge Gluing:
Side Precision: After side planing, straightness must be ≤0.1mm/m (i.e., lateral bending deviation within 0.1mm over 1m length). Otherwise, the panel surface will develop "waviness."
Color Matching (Wood Color Matching): Furniture-grade glulam requires color difference ΔE≤1.5 between adjacent strips (barely discernible to the naked eye under normal lighting) to ensure uniform panel surface color. Structural glulam has no special color requirements.
Moisture Content Consistency: Moisture content deviation between strips before edge-gluing must be ≤±1.5%. Otherwise, differential shrinkage/swelling in different directions will cause cracking.
3.3 Surface Treatment (Sanding and Finishing)
After edge-gluing, the rough glulam panel requires surface sanding:
Rough Sanding (60-80 grit): Removes glue lines, saw marks, and minor unevenness from edge-gluing.
Fine Sanding (150-240 grit): Achieves smooth, uniform surface (Ra≤3.2μm), ensuring adhesion for subsequent paint or hard wax oil finishes.
Thickness Tolerance Control: Finished product thickness deviation controlled within ±0.2mm, far superior to ordinary solid sawn timber (±0.5-1.0mm).
IV. Adhesive Systems for Glulam
4.1 Adhesive Types and Applications
Adhesive selection for glulam is determined by both product use (structural/non-structural) and environmental grade requirements:
| Adhesive Type | Applicable Products | Characteristics | Environmental Grade Potential | Curing Conditions |
|---|---|---|---|---|
| Melamine-Modified Urea-Formaldehyde (MUF) | Non-structural glulam (interior furniture) | Fast curing (hot/cold press both possible), good bonding strength, moderate cost | E0 (≤0.025mg/m³) | Cold press (20-30°C) 2-6h or hot press (100-120°C) 5-10 min |
| Aqueous Polymer Isocyanate (API) | Non-structural/light structural glulam | Good water resistance, excellent strength, formaldehyde-free (note: API formulations may contain trace free MDI) | ENF (HENF requires VOC verification) | Cold press (20-30°C) 4-12h or hot press (80-100°C) |
| Resorcinol-Formaldehyde Resin (PRF) | Structural glulam (building beams/columns) | Extremely high bonding strength and weather resistance (exterior grade), long-term resistance to moisture and temperature variation, but dark color (reddish-brown glue line), high cost | Typically E0 (formaldehyde emission slightly higher than MUF but can meet E0 through formulation optimization) | Room-temperature cure (20-30°C) 8-24h, or low-temperature (40-60°C) acceleration |
| MDI (Isocyanate) Adhesive | Structural/non-structural (premium formaldehyde-free) | Formaldehyde-free, excellent water resistance, extremely high strength, fast curing, but moisture-sensitive, high cost (3-5x UF) | ENF/HENF (zero formaldehyde addition) | Hot press (140-170°C) 3-15 min or cold press (20-30°C) 12-24h |
| Epoxy Resin Adhesive | Special structures/high-demand | Extremely high strength, excellent chemical resistance, but extremely high cost, demanding application requirements | E0 | Cold press (20-30°C) 24-72h |
JINDIWOOD Glulam Adhesive Strategy:
Non-Structural Furniture Grade: Uses MUF adhesive with formaldehyde scavenger dual technology. Standard products stably achieve E0, with custom options up to ENF.
Structural Construction Grade: Uses PRF or MDI adhesives, meeting stringent requirements for outdoor environments and long-term load-bearing.
4.2 Effect of Adhesives on Glulam Performance
| Adhesive Type | Finger Joint Tensile Strength (MPa) | Wet Bond Strength Retention | Weather Resistance (Outdoor Exposure) | Applications |
|---|---|---|---|---|
| MUF | 12-18 | ≥70% (4h boiling) | Moderate (interior only) | Interior furniture, cabinets, wooden doors |
| API | 14-20 | ≥80% | Good (short-term outdoor) | Interior/exterior decoration, light structures |
| PRF | 18-25 | ≥90% | Excellent (long-term outdoor) | Building beams/columns, bridges, outdoor timber structures |
| MDI | 20-28 | ≥90% | Excellent (long-term outdoor) | Structural glulam, outdoor furniture |
V. Classification and Grades of Glulam
5.1 By Application
| Category | Grade Code | Characteristics | Typical Applications |
|---|---|---|---|
| Non-Structural Glulam (Furniture Grade) | GL (Interior Grade) | Focus on appearance (color, grain, joints), high environmental grades (E0/ENF), moderate mechanical properties | Solid wood furniture, cabinets, wooden doors, staircases, countertops, decorative moldings |
| Structural Glulam (Construction Grade) | GL (Structural Grade) | Focus on mechanical properties (strength class grading), good weather resistance, high bonding strength, lower appearance requirements | Long-span timber beams, gymnasium arches, bridges, timber building columns/beams |
| Decorative Glulam | GL (Decorative Grade) | Emphasis on attractive grain, no color variation, fine joints, multiple sanding passes | Interior wall cladding, feature walls, ceilings |
5.2 By Appearance Grade (GB/T 21140-2024 Finger-Jointed Timber — Non-Structural)
The appearance grade of non-structural glulam is classified based on the number and extent of defects:
| Grade | Defect Allowance | Applications |
|---|---|---|
| Premium | No knots (or minimal live knots, ≤5mm diameter, ≤1 piece/m), no cracks, no discoloration, uniform joints (width ≤0.1mm) | High-end furniture, countertops, door panels, decorative moldings |
| First Class | Limited sound live knots (≤10mm diameter, ≤3 pieces/m), very slight cracks (length ≤20mm, depth ≤1mm), slight color variation | Standard furniture, cabinets, stair treads |
| Qualified | Certain number of knots (including dead knots but filled, ≤20mm diameter, ≤5 pieces/m), cracks (length ≤50mm, depth ≤2mm), obvious color variation | Interior structural components, non-appearance uses |
VI. Core Technical Specifications of Glulam
6.1 Physical and Mechanical Performance Requirements
Non-Structural Glulam (GB/T 21140-2024 Requirements):
| Performance Indicator | Unit | Requirement | Test Method |
|---|---|---|---|
| Moisture Content | % | 6-12 | GB/T 17657 (gravimetric) |
| Bonding Strength (finger joint) | MPa | ≥6.0 (hardwood) / ≥4.0 (softwood) | GB/T 17657 (tensile shear) |
| Modulus of Rupture (MOR) | MPa | ≥30 (longitudinal) | GB/T 17657 (3-point bending) |
| Modulus of Elasticity (MOE) | MPa | ≥6000 (longitudinal) | GB/T 17657 |
| Immersion Delamination | — | Delamination rate ≤5% (no significant glue line opening at finger joints) | Immersion test (specimen immersed in water at 63±3°C, dried, then measured for glue line delamination) |
| Formaldehyde Emission | mg/m³ | E0 ≤0.025 / ENF ≤0.015 | GB/T 17657 (chamber method) |
Structural Glulam (GB/T 26899-2022 Structural Glued Laminated Timber Requirements — Strength Class Examples):
| Strength Class | Characteristic Bending Strength (MPa) | Characteristic MOE (MPa) | Characteristic Tensile Strength (MPa) | Characteristic Compressive Strength (MPa) |
|---|---|---|---|---|
| GL20 | 20 | 7500 | 12 | 18 |
| GL24 | 24 | 8400 | 14 | 21 |
| GL28 | 28 | 9500 | 16 | 24 |
| GL32 | 32 | 10500 | 19 | 27 |
Relationship Between Strength Class and Species:
GL20/GL24 grades are typically made from softwood species such as pine, fir, and poplar.
GL28/GL32 grades require hardwood species such as beech, oak, and eucalyptus, or higher lamination ratios and high-performance adhesives (e.g., PRF/MDI).
6.2 Tensile Strength Assurance at Finger Joints
Finger joints are the "weak link" in glulam, with tensile strength typically at 70-90% of the parallel-to-grain tensile strength of non-jointed wood.
Measures to Ensure Finger Joint Strength Compliance:
Finger Geometry Precision Control: Tooth geometry deviations (length, width, pitch) within ±0.1mm.
High-Toughness Adhesives (API/PRF): The adhesive layer can elastically deform with wood shrinkage/swelling, preventing stress concentration and glue line cracking.
In-Line Destructive Testing: For each production batch (e.g., every 500 pieces), 1 piece is tested for tensile strength at the finger joint to ensure wood failure ≥75%.
VII. Surface Treatment and Coating of Glulam
7.1 Surface Treatment
After sanding, glulam surfaces can be directly coated without the need for "sealer primer" treatment required for MDF or particleboard. Glulam is a natural solid wood substrate without porosity issues (although it has vessel grooves, overall paint absorption is uniform, without "suction" or "pinhole" defects).
Surface Treatment Process:
Fine Sanding: 180-240 grit abrasive, Ra≤3.2μm.
Dust Removal: High-pressure air blow-off or electrostatic dust removal.
Base Color Adjustment (optional): Adjust areas with significant color variation using ground coat for uniform overall appearance.
Coating: Direct application of PU, UV, water-based paints, hard wax oil, or clear varnish.
7.2 Recommended Coating Solutions
| Coating Type | Characteristics | Style | Applicable Grade |
|---|---|---|---|
| Clear Varnish (PU/Water-based) | Preserves natural wood grain and color, natural texture | Nordic, Japanese, Neo-Chinese | Premium/First Class |
| Open-Pore Finish (Hard Wax Oil/Water-based) | Open grain structure, realistic tactile feel, matte surface, extremely eco-friendly | Natural, Rustic | Premium (requires high-quality grain) |
| Closed-Pore Finish (PU/UV High-gloss/Matte) | Smooth surface, controlled gloss (10-95GU), scratch-resistant, easy to clean | Modern minimalism, Light luxury | All grades (closed finish can mask minor defects) |
| Colored Coating (PU/UV Pigmented) | Covers natural wood color, any color possible | Modern, Custom | All grades (completely masks color variation and knots) |
VIII. Application Scenarios of Glulam
8.1 Furniture Manufacturing
Glulam is increasingly widely used in high-end solid wood furniture and custom furniture:
| Application | Recommended Grade | Typical Thickness (mm) | Selection Rationale |
|---|---|---|---|
| Solid wood dining/desk tops | Premium (hardwood/oak/walnut) | 25-40 | Large sizes, defect-free, attractive grain, dimensionally stable (no cracking) |
| Solid wood kitchen cabinet doors | First Class (medium-density/hardwood) | 18-22 | Eco-friendly (E0/ENF), superior moisture resistance to MDF, versatile coating options |
| Wardrobe/walk-in closet shelves | First Class (medium-density/poplar/pine) | 18-25 | Good load-bearing (MOR≥30MPa), excellent nail-holding, no deformation |
| Wooden door frames | First Class (pine/fir) | 30-40 | Dimensionally stable (no cracking/twisting), lightweight (finger jointing allows use of light species) |
| Stair treads | Premium (hardwood/oak/beech) | 30-50 | High hardness, high strength, wear-resistant, width up to 300-500mm through edge-gluing |
| Musical instruments/speakers | Premium (specific hardwoods/maple/walnut) | 15-30 | Uniform density and vibration properties; finger jointing ensures stability and consistency of large components |
Comparison: Glulam vs. Solid Sawn Timber in Furniture Applications:
| Comparison Dimension | Glulam (Furniture Grade) | Solid Sawn Timber (Directly from Logs) |
|---|---|---|
| Maximum Width | Up to 1200mm (via edge-gluing) | Depends on log diameter (typically ≤300-400mm) |
| Maximum Length | Up to 6000mm (via finger jointing) | Depends on log length (typically ≤2000-4000mm) |
| Knots/Defects | Completely removed (or very few retained) | Present (requires cutting out, reducing yield) |
| Warping/Cracking Risk | Extremely low (uniform MC, internal stress eliminated) | Higher (significant anisotropy, prone to deformation) |
| Grain Continuity | Interrupted at joints | Naturally continuous (root to tip) |
| Price | Moderate (uses small-diameter logs, lower cost) | High (depends on large-diameter defect-free logs) |
| Environmental Grade | Up to ENF (MDI adhesive) | Natural (adhesive-free) |
8.2 Building and Structural Applications
Structural glulam applications in timber construction represent a landmark achievement in modern engineered wood products:
| Structural Component | Typical Size | Strength Grade Requirement | Functional Characteristics |
|---|---|---|---|
| Long-span beams (straight/curved) | Section 100×200mm to 200×600mm, span 6-30m | GL24-GL32 | Extremely high strength, lightweight (approx. 1/6 of reinforced concrete), can be curved |
| Timber columns | Section 100×100mm to 200×300mm, height 3-12m | GL20-GL28 | High compressive strength, superior fire resistance to steel (char layer insulation), attractive appearance |
| Arch structures (gymnasiums, exhibition halls) | Span up to 50-100m (glued arches) | GL28-GL32 (special design) | Elegant form, strong spatial presence, fast construction |
| Bridge structures | Span up to 30-60m (glued timber bridges) | GL32+ (special design) | Lightweight, corrosion-resistant, good seismic performance, lower maintenance than steel bridges |
Advantage Comparison of Structural Glulam:
| Structural Material | Strength/Weight Ratio | Fire Resistance | Seismic Performance | Construction Speed | Carbon Footprint |
|---|---|---|---|---|---|
| Structural Glulam | High (1.5-2x concrete) | Excellent (char layer insulates) | Excellent (flexible energy dissipation) | Fast (prefabricated assembly) | Low (carbon sequestration) |
| Reinforced Concrete | Moderate (dense) | Good (non-combustible) | Moderate (requires special design) | Slower (cast in place) | High (cement CO₂ emissions) |
| Steel Structure | High (but dense) | Poor (softens at high temperature) | Good | Moderate | High (steelmaking CO₂ emissions) |
8.3 Interior Decoration
Glulam is increasingly used in interior decoration, especially for spaces pursuing "solid wood feel, natural style":
Feature Walls/Wall Paneling: Large-size glulam panels (width 600-1200mm, length 2400-3000mm), showcasing continuous natural wood grain without nail holes or visible joints.
Ceilings: Thin glulam panels (12-18mm), installed as slatted grids or full panels, creating a warm, natural spatial atmosphere.
Window Frames/Door Frames/Baseboards: Slender sections (width 80-200mm), with finger jointing ensuring continuous length (no splicing required).
Stair Treads/Handrails: High-hardness hardwood glulam (oak/beech), tread width up to 300-500mm (edge-gluing), handrail length up to 4000mm (finger jointing).
8.4 Special Industrial Applications
Musical Instrument Manufacturing: Piano soundboards (spruce glulam, requiring extremely high acoustic consistency and longitudinal MOE), guitar necks (mahogany or maple glulam), violin backs (selected hardwood, zero tolerance for knots).
Sports Equipment: Ski cores, surfboards, bowling alleys (hard maple glulam, requiring extremely high hardness and wear resistance).
Molds/Models: Precision casting wood patterns, architectural models (requiring high dimensional accuracy, smooth surfaces, and deformation resistance).
IX. Common Quality Misconceptions and Facts
Misconception 1: "Glulam is just glued scraps of wood, definitely not as good as solid wood."
Fact: The essence of glulam is "upcycling inferior timber." Through industrial processing to eliminate natural defects and reorganize structure, its mechanical properties and dimensional stability surpass the original solid wood.
Strength: Although finger joints are slightly weaker than defect-free wood (approx. 70-90%), the overall panel's average strength exceeds natural solid wood containing knots, cross-grain, cracks, and other defects. In engineering applications, glulam's design strength values even exceed those of some low-grade natural sawn timber.
Stability: Glulam has uniform moisture content (overall deviation ≤±1.5%), uniform shrinkage/swelling in all directions, and warping/cracking risk far lower than natural solid wood.
Appearance: Premium-grade glulam (no knots, no color variation, fine joints) can achieve or even surpass the appearance quality of most natural solid sawn timber.
Misconception 2: "Glulam is not eco-friendly and contains formaldehyde."
Fact: Glulam's environmental grade is entirely determined by the adhesive — MUF (E0) and MDI (ENF/HENF) adhesives are now widely used, with formaldehyde emissions as low as ≤0.015mg/m³, even lower than some natural woods (wood itself emits trace amounts of formaldehyde). When purchasing, look for test reports and environmental grade labels (E0/ENF/HENF) — it's unrelated to choosing "glulam" or "solid wood" as a category.
Misconception 3: "Finger joints in glulam break easily."
Fact: Although finger joint tensile strength is lower than non-jointed wood (approx. 70-90%), under normal furniture use loads (e.g., tabletops bearing 5-10kg/m² uniform load), the safety factor at finger joints typically exceeds 4-6 times (i.e., actual tensile strength is 4-6 times the design stress). Only under long-term heavy loads (e.g., heavy shelving, bridges) or impact loads (e.g., industrial environments with frequent collisions) is special attention needed for finger joint load-bearing capacity — precisely the issue that structural glulam addresses through increased finger joint length (tooth length increased to 20-40mm) and use of high-performance adhesives (PRF/MDI).
Misconception 4: "Glulam is expensive with low cost-performance ratio."
Fact: Raw materials for glulam (small-diameter, low-quality timber) cost far less than large-diameter defect-free logs, but processing costs (drying, finger jointing, edge-gluing, sanding) are higher. Overall comparison:
Compared to solid sawn timber: At the same specifications, glulam costs only 40-60% of solid sawn timber of the same species and grade (e.g., a 200mm wide, 3000mm long solid oak tabletop is far more expensive than an oak glulam tabletop, and the latter is more stable).
Compared to other engineered wood: Glulam costs higher than MDF and particleboard (approx. 1.5-2.5x), but its "solid wood texture" and "repairability" (surface scratches can be sanded and refinished) cannot be replicated by other engineered wood products.
X. Technology Development Trends of Glulam
10.1 Expansion of Structural Glulam Applications
With the deepening implementation of China's General Code for Timber Structures (GB 55005) promulgated in 2023, and growing societal consensus on "dual carbon" goals, timber construction is entering a new development phase in China. Applications of structural glulam in long-span public buildings (exhibition halls, gymnasiums, airports), multi-story timber residential buildings (3-6 stories), and hybrid structures (timber-steel/timber-concrete composite) will continue to grow. China's annual production of structural glulam is expected to increase by over 50% by 2030 compared to 2025.
10.2 Formaldehyde-Free and Green Manufacturing
MDI Adhesive Adoption in Non-Structural Glulam: With increasing domestic MDI production capacity (Wanhua Chemical and others) and decreasing costs (prices down 30-40% from 2020), ENF-grade glulam will gradually become the standard specification for high-end furniture and interior decoration.
Development of Bio-Based Adhesives: Lignin-based and tannin-based adhesives for glulam are entering pilot-scale production, with potential to partially replace fossil-based adhesives within the next 5-10 years, further reducing carbon footprint.
Water-Based Coatings Replacing Solvent-Based Coatings: In glulam coating, the proportion of water-based paints, UV-LED curing coatings, and hard wax oils continues to rise (from under 20% in 2020 to over 45% in 2025), significantly reducing VOC emissions.
10.3 High Performance and Customization
High-Strength Glulam (>GL35): Through selection of high-strength species (eucalyptus, birch, acacia — domestic fast-growing high-strength species), optimized finger joint geometry (increased tooth length and count), and high-performance adhesives (PRF/MDI), developing GL35 and higher structural glulam grades to expand applications in high-rise timber construction.
Glulam-LVL Hybrid: Combining Laminated Veneer Lumber (LVL) with glulam through composite bonding, achieving higher strength, longer spans, and greater design flexibility.
Customized Finger Jointing/Edge Gluing (Just-in-Time Production): With the proliferation of flexible manufacturing and digital production scheduling, glulam production is shifting from "mass production of standard sizes" to "customer-specified dimensions + small-batch, multi-variety" models, meeting the demands of whole-house customization and personalized design.
10.4 Digital and Intelligent Quality Control
In-Line Acoustic Testing: Using acoustic resonance methods (stress wave or ultrasonic) for non-destructive in-line testing of each finger-jointed piece. Based on resonance frequency and damping coefficient, real-time assessment of finger joint strength and internal defects (cracks, adhesive defects), achieving 100% full inspection and replacing traditional manual sampling.
AI Color Sorting: Machine vision and deep learning-based color recognition systems for automatic color grading of each wood strip before edge-gluing (ΔE automatically calculated). Automatic matching of different color grades to achieve optimal uniformity of finished panel surface color.
Digital Traceability System: Each glulam product is assigned a unique QR code or RFID tag, recording all raw material batches (species, drying records, moisture content), production information (finger joint parameters, adhesive batch, hot press curve), and quality test results — achieving full life-cycle traceability from log to finished product.

JINDIWOOD · Engineered for Certainty — Every short piece recombined through finger jointing builds a foundation of certainty for the strength of furniture and the safety of buildings.
This article is an original technical publication by JINDIWOOD. Reproduction must indicate the source.