中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
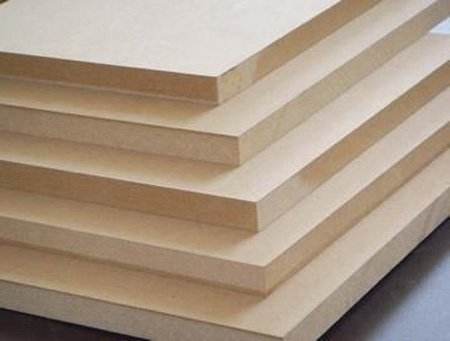
I. Basic Concept of MDF
Medium Density Fiberboard (MDF) is a wood-based panel with a density between 650 and 800 kg/m³, made from wood fibers or other plant fibers through fiber preparation, adhesive application, mat forming, and hot pressing.
Unlike plywood (cross-laminated veneers) and particleboard (glued and pressed particles), the essential characteristic of MDF is that wood is reduced to a fibrous state and then reconstituted into a panel. This process completely eliminates natural wood defects such as knots, grain direction, and growth stresses, making MDF the most homogeneous and flattest wood-based panel, particularly suitable for surface finishing (melamine paper, wood veneer, painting, etc.).
Key Data: High-quality MDF achieves internal bond strength of 0.6–1.2 MPa, modulus of rupture of 25–40 MPa, and surface flatness tolerance within ±0.15 mm, making it the preferred substrate for furniture manufacturing and interior decoration.
II. Raw Material System of MDF
2.1 Wood Fiber Raw Materials
MDF can be made from a wide range of raw materials, including wood processing residues, fast-growing wood, branches, etc. Raw material selection directly affects panel color, fiber morphology, and physical properties.
| Raw Material Type | Fiber Morphology | Panel Characteristics | Main Applications |
|---|---|---|---|
| Poplar | Fine, long fibers, thin walls | Light color, uniform texture | High-end furniture, decorative panel substrate |
| Pine | Longer fibers, higher resin content | Good strength, yellowish color | Structural MDF, packaging |
| Eucalyptus | Medium fibers, higher density | High strength, medium color | Load-bearing furniture, flooring substrate |
| Mixed hardwoods | Varying fiber lengths | Balanced performance, lower cost | General-purpose MDF |
| Agricultural straw | Short fibers, high ash content | Slightly lower performance, eco concept | Low-cost eco panels |
JINDIWOOD Technical Standard: All MDF raw materials use virgin poplar. Thin panels (≤9 mm) achieve density ≥830 kg/m³, thick panels (>9 mm) ≥750 kg/m³, far exceeding conventional market products, ensuring excellent machining performance and surface quality.
2.2 Adhesive Systems
Common MDF adhesives are similar to those for plywood, but due to the large specific surface area of fibers (hundreds of times that of veneers), application rates and adhesive types differ:
| Adhesive Type | Application Rate (% dry fiber) | Environmental Grade | Applications |
|---|---|---|---|
| Urea-formaldehyde (UF) | 8–12% | E1/E0 | General indoor furniture |
| Melamine-modified urea-formaldehyde (MUF) | 10–14% | E0/ENF | Mid-to-high-end furniture, moisture-resistant panels |
| Isocyanate (MDI) | 4–6% | ENF/HENF | Formaldehyde-free panels, children's furniture |
| Soy protein adhesive | 10–15% | ENF | Eco-friendly MDF |
MDF adhesive application differs from plywood—the adhesive is atomized and mixed with fibers in a high-speed blender. The adhesive must have low viscosity and high penetration to uniformly coat each fiber.
2.3 Auxiliary Additives
Paraffin emulsion (water repellent): 0.5–1.5% of dry fiber, improves moisture resistance
Curing agent (ammonium chloride, etc.): accelerates adhesive curing, shortens hot pressing time
Flame retardant (phosphorus-nitrogen): imparts fire resistance, up to B1–C grade
Anti-mold agent: inhibits mold growth, suitable for humid environments
III. MDF Production Process
3.1 Chipping and Screening
Logs or wood residues are processed into calibrated chips (length 15–30 mm, thickness 3–5 mm) by a chipper. A vibrating screen removes oversized, undersized, and impurities (sand, metal) to ensure uniform material entering the refiner.
Key Control Point: Uneven chip size causes fluctuations in fiber separation quality. Too large increases refining energy and produces coarse fibers; too small is prone to carbonization.
3.2 Fiber Preparation — Thermo-Mechanical Refining (Core Step)
This is the most essential step distinguishing MDF from other wood-based panels. Chips undergo a combined "cooking + refining" treatment in a refiner:
Step 1: Pre-cooking
Chips enter a vertical preheater, exposed to high-temperature steam (pressure 0.8–1.2 MPa, temperature 160–180°C)
Cooking time: 3–8 minutes (adjusted by wood species and chip thickness)
Steam softens lignin (natural binder in wood), reducing bonding forces between fibers
Step 2: Refining
Cooked chips enter the refining chamber; shear forces between the high-speed rotating disc and stationary disc tear chips into individual fibers
Disc gap: 0.1–0.5 mm (adjustable)
Paraffin emulsion (water repellent) and sizing agent injected into the refining chamber (some processes add adhesive here)
Core Principle: Thermo-mechanical refining uses the synergistic effect of steam thermal energy and mechanical shear to separate chips into individual fibers without severely cutting them. The longer the fibers are retained, the higher the panel strength.
After refining, fibers have moisture content as high as 50–60% and are fluffy, requiring immediate drying.
3.3 Fiber Drying
Wet fibers are pneumatically conveyed to a dryer, where hot air reduces moisture content to the process range.
Drying Method: Pneumatic pipe drying (three-pass dryer) or flash drying
Heat Source: Hot air furnace (biomass/natural gas) providing 160–200°C hot air
Moisture Content After Drying: 8–12% (target before mat forming)
Drying Time: Only 2–5 seconds (instantaneous in high-speed hot air)
Technical Difficulty: Fiber drying is fast with short residence time, requiring precise control of hot air temperature and velocity. Too high—surface carbonization, darker color, strength reduction; too low—high moisture content, difficult mat forming, blistering during hot pressing.
Dried fibers are collected by cyclone separator and enter the blending process through a metering bin.
3.4 Blending — Uniform Mixing of Fibers and Adhesive
Blending is the core step of the dry process. Dried fibers are precisely metered by electronic belt scale, then enter a high-speed blender (blender), where adhesive is added by atomized spraying, along with curing agent and water repellent (paraffin emulsion).
| Process Parameter | Typical Value | Control Point |
|---|---|---|
| Resin loading | 8–14% (% dry fiber) | Too low → insufficient internal bond; too high → higher cost, longer pressing cycle |
| Adhesive solid content | 50–65% | Affects blending uniformity and penetration |
| Mixing speed | 500–1500 rpm | Ensures adhesive uniformly coats each fiber |
| Paraffin addition | 0.5–1.5% | Affects thickness swelling rate |
Moisture Content After Blending: Increases to 12–16% due to water in the adhesive, preparing for mat forming and hot pressing.
3.5 Mat Forming
Blended fibers are uniformly spread by a forming machine onto a continuously moving steel belt or caul plate to form a fiber mat with a certain thickness and density.
Two main forming methods:
Air forming: Fibers are suspended in an air stream and deposited by gravity and airflow; suitable for graded-structure MDF (fine fibers in surface, coarse fibers in core), producing a smooth surface
Mechanical forming: Distribution by mechanical rollers or oscillating hoppers; simpler structure, suitable for homogeneous panels
Pre-pressing after forming: The mat is pressed at 0.5–1.0 MPa by a continuous pre-press, compacting the loose fiber mat to 1/3–1/2 of its original thickness, improving mat strength and thermal conductivity for entry into the hot press.
3.6 Hot Pressing (Core Step)
Under high temperature and pressure, the mat undergoes adhesive curing → fiber densification → panel shaping. This is the final step determining MDF density, strength, thickness precision, and environmental grade.
Three Key Stages of the Hot Pressing Cycle:
| Stage | Pressure | Temperature | Function |
|---|---|---|---|
| Stage 1: Compression | Rapid rise to 3.0–4.5 MPa | 160–220°C | Rapidly compresses mat, expels air and moisture, fibers begin plastic deformation |
| Stage 2: Curing | Maintain 2.0–3.5 MPa | Constant | Adhesive cross-links and cures, forming strong bonds between fibers |
| Stage 3: Venting/Depressurization | Gradient decrease to 0 | Natural cooling | Releases internal steam pressure, prevents blistering, shapes panel |
Empirical Formula for Pressing Cycle and Panel Thickness:
Total pressing time (seconds) ≈ Panel thickness (mm) × 8–15 s/mm
For 18 mm MDF, the pressing cycle is approximately 150–270 seconds (2.5–4.5 minutes), including:
Compression: 15–30 seconds
Curing: 100–200 seconds
Venting: 20–40 seconds
Key Control Technologies:
Thickness control: Hot press equipped with thickness gauges, precisely controlling finished panel thickness, tolerance ±0.15 mm
Temperature gradient control: Temperature difference between mat surface and core should not be too large (≤20°C), otherwise causing "surface cured, core uncured"—surface cured while core adhesive has not fully reacted
3.7 Post-Treatment
Cooling and conditioning: Panels exiting the hot press are as hot as 80–120°C, requiring natural cooling to room temperature by a panel turner/cooler. Cooled panels are stored in the warehouse for 48–72 hours for conditioning, allowing internal stresses to fully release and moisture content to equilibrate with the environment, preventing warping during subsequent processing.
Sanding: Conditioned panels are sanded by wide-belt sander:
First pass: Coarse sanding (60–80 grit) — removes surface carbonized layer and thickness unevenness
Second pass: Medium sanding (100–120 grit) — flattens panel surface
Third pass: Fine sanding (150–180 grit) — precision grinding to meet finishing requirements
Sanding amount is typically 0.5–1.5 mm (both sides combined), after which panel thickness reaches final specification, surface roughness Ra ≤3.2 μm.
Cutting: Trimmed to standard dimensions (e.g., 1220×2440 mm), removing irregular edges.
Grading and Packaging: Sorted by appearance grade, packaged and stored.
IV. Core Technical Indicators and Testing Methods of MDF
4.1 Density
Density is the most basic physical indicator of MDF, directly affecting mechanical strength and machining performance.
Density Range (GB/T 11718-2021): 650–800 kg/m³ (medium density)
Testing Method: Weighing method (precisely measuring specimen mass and volume)
JINDIWOOD Standard: Thin panels (≤9 mm) ≥830 kg/m³, thick panels (>9 mm) ≥750 kg/m³
Effect of Density on Performance:
Too low → insufficient strength, poor screw holding, porous surface
Too high → severe tool wear, overweight panels, increased cost
Uneven → "hard and soft spots" after sanding, affecting finishing effect
4.2 Internal Bond Strength (IB)
Internal bond strength is the core indicator measuring the bonding fastness between fibers inside MDF, reflecting the panel's resistance to internal separation.
Testing Method: Cut 50×50 mm specimens from the panel, bond special metal fixtures to both sides, apply tensile load perpendicular to the panel surface via tensile testing machine, record maximum load at failure, divide by specimen area to obtain IB value (MPa).
GB/T 11718-2021 Requirements:
Standard: IB ≥ 0.55 MPa
Furniture: IB ≥ 0.65 MPa
Load-bearing: IB ≥ 0.80 MPa
Influencing Factors:
Resin loading: IB increases with resin loading (but there is an economic upper limit)
Fiber morphology: Longer, more intact fibers yield higher IB
Hot pressing parameters: Synergistic coordination of temperature, pressure, and time
4.3 Modulus of Rupture (MOR) and Modulus of Elasticity (MOE)
Like plywood, MOR and MOE are key mechanical indicators measuring panel load-bearing capacity.
Testing Method: Three-point bending (specimen span is 20 times thickness, uniformly loaded to failure)
GB/T 11718-2021 Requirements:
MOR ≥ 23 MPa (standard) / ≥ 30 MPa (load-bearing)
MOE ≥ 2700 MPa (standard) / ≥ 3500 MPa (load-bearing)
MDF has lower MOR than high-quality plywood (fibers are short, while plywood uses continuous long veneers), but its surface flatness and thickness uniformity are far superior to plywood, giving it irreplaceable advantages in surface finishing applications.
4.4 Thickness Swelling (TS)
This is the core indicator measuring MDF moisture resistance, especially important for humid environments such as kitchens and bathrooms.
Testing Method: 50×50 mm specimens immersed in water at 20±2°C for 24 hours, measuring thickness change rate before and after immersion
GB/T 11718-2021 Requirements: 24-hour thickness swelling ≤15% (standard) / ≤10% (moisture-resistant)
Technical Means to Reduce Swelling:
Add paraffin emulsion and other water repellents
Increase hot pressing temperature and time (increase fiber plastic flow, reduce capillaries)
Use melamine-modified adhesive (MUF)
4.5 Formaldehyde Emission
MDF has relatively high adhesive usage (8–14%), making formaldehyde emission control particularly important. Testing methods are consistent with plywood.
| Environmental Grade | Formaldehyde Emission (Climate Chamber Method, mg/m³) |
|---|---|
| E1 (National Mandatory Standard) | ≤0.050 |
| E0 | ≤0.025 |
| ENF | ≤0.015 |
4.6 Surface Roughness
This is a quality control indicator unique to MDF, directly related to finishing quality (melamine paper, veneer, paint) and bonding strength.
Testing Method: Stylus roughness tester measuring Ra value
JINDIWOOD Standard: Surface roughness Ra ≤3.2 μm after sanding
Effect of Surface Roughness on Processing:
Ra too high (rough surface) → Increased adhesive usage during lamination, possible "white spots" or "pitting"
Ra too low (over-sanded) → Surface too dense, poor adhesive penetration, reduced lamination adhesion
V. Common Classifications and Grades of MDF
5.1 Classification by Density Grade (GB/T 11718-2021)
| Category | Density Range (kg/m³) | Typical Applications |
|---|---|---|
| Lightweight MDF | < 650 | Non-load-bearing decoration, model making |
| Medium Density MDF (Standard) | 650–800 | Furniture, decoration, decorative panel substrate |
| High Density MDF (HDF) | > 800 | Flooring substrate, high-strength furniture |
5.2 Classification by Application
| Type | Core Requirement | Typical Applications |
|---|---|---|
| Furniture (Standard) | IB ≥0.65 MPa, fine surface | Wardrobes, cabinets, tables and chairs |
| Load-bearing | MOR ≥30 MPa, higher density | Shelves, office desks, door panels |
| Moisture-resistant | Thickness swelling ≤10% | Bathroom cabinets, kitchen furniture |
| Flame-retardant | Fire rating B1–C | Public space decoration, hotels |
| Low formaldehyde (ENF) | Formaldehyde emission ≤0.015 mg/m³ | Children's furniture, bedrooms |
5.3 Classification by Appearance Grade
MDF appearance grades are mainly divided by the number and size of surface defects (black spots, glue spots, indentations, scratches, carbonization points, etc.):
Premium: No visible surface defects, suitable for high-quality finishing
First Grade: A few minor defects allowed, suitable for general finishing
Qualified: A certain number of defects allowed, suitable for applications where they will be covered or invisible after lamination
Common Surface Defects After Sanding and Their Causes:
| Defect Type | Typical Manifestation | Possible Cause |
|---|---|---|
| Black spots | Black dots scattered on panel surface | Refining temperature too high or bark/impurities not removed from raw material |
| White spots/glue spots | Local whitening or hard lumps on surface | Uneven blending or local adhesive accumulation during hot pressing |
| Sanding marks | Parallel grooves on surface | Sanding belt grit too coarse or uneven wear |
| Carbonization points | Black scorched spots | Hot pressing temperature too high or local fiber overheating |
VI. Comparative Analysis of MDF and Plywood
| Comparison Dimension | MDF | Plywood |
|---|---|---|
| Structure | Uniform fiber distribution, isotropic | Cross-laminated veneers, more anisotropic |
| Surface flatness | Excellent, suitable for fine finishing | Good, but visible veneer joints |
| Edge treatment | Dense edges, can be machined into profiles | Layered structure visible at edges, requires edge banding |
| Screw holding | Good (face), but loosens after repeated screwing | Excellent, especially edge screw holding |
| MOR | Medium (25–40 MPa) | High (50–100 MPa) |
| Moisture resistance | Poor (high thickness swelling) | Good (waterproof adhesives available) |
| Environmental performance | High adhesive usage, formaldehyde control difficult | Relatively lower adhesive usage |
| Price | Lower (same grade comparison) | Higher |
| Typical applications | Decorative panel substrate, furniture components, carving | Load-bearing structures, construction formwork, flooring substrate |
VII. Common Quality Problems and Cause Analysis of MDF
7.1 Thickness Deviation and Uneven Density
Phenomenon: Large thickness variation within the same panel, or inconsistent thickness in the same batch.
Possible Causes:
Improper setting or wear of hot press thickness gauges
Uneven fiber distribution during mat forming (thick and thin)
Insufficient parallelism of hot press platens or platen deformation
Solutions: Regularly calibrate hot press thickness gauges, optimize mat forming uniformity, regularly maintain hot press parallelism.
7.2 Insufficient Internal Bond Strength
Phenomenon: Panels easily delaminate, severe "powdering" during surface sanding, rough edges when cutting.
Possible Causes:
Insufficient resin loading or substandard adhesive quality
Low hot pressing temperature or insufficient curing time
Poor fiber morphology (over-refining resulting in too short fibers)
Insufficient curing agent addition
Solutions: Optimize blending process, adjust hot pressing parameters, regularly test adhesive gel time.
7.3 Excessive Thickness Swelling
Phenomenon: Panel thickness significantly increases in humid environments or water immersion tests, even producing "mushroom-like" deformation.
Possible Causes:
Insufficient paraffin (water repellent) addition or uneven dispersion
Low panel density (many internal pores)
Insufficient hot pressing cycle, incomplete adhesive curing
Solutions: Increase paraffin dosage and optimize spray dispersion, moderately increase panel density, extend hot pressing time.
7.4 Warping Deformation
Phenomenon: Panel presents tile-like or bow-shaped bending after placement.
Possible Causes:
Excessive or uneven sanding (destroying symmetrical structure)
Large difference between finished panel moisture content and use environment
Insufficient conditioning time, internal stresses not fully released
Obvious density gradient asymmetry during mat forming
Solutions: Control sanding amount (not exceeding 0.5 mm per side), sufficient conditioning to balance moisture content, optimize mat forming uniformity.
7.5 Surface Blistering
Phenomenon: Local bulges on panel surface, internal cavities or delamination visible when cut with a blade.
Possible Causes:
Too fast venting at the end of hot pressing, internal steam pressure not fully released
Excessive moisture content of veneer (or fiber mat)
Improper hot pressing temperature setting, surface cured while core uncured
Solutions: Extend venting stage time, reduce mat moisture content, optimize hot pressing temperature curve.
VIII. Technical Development Trends of MDF
8.1 Formaldehyde-Free
Technical breakthroughs in MDI formaldehyde-free adhesives and bio-based adhesives have driven continuous improvement in MDF environmental grades. HENF-grade MDF (formaldehyde emission ≤0.015 mg/m³) has entered mass production and will gradually become mainstream.
8.2 Lightweight and High-Strength
Through fiber modification, foaming technology, or gradient density structure design, panel weight is reduced (density ≤600 kg/m³) while maintaining sufficient mechanical strength, meeting lightweight application needs such as automotive interiors and aircraft cabins.
8.3 Functionalization
Flame-retardant MDF: Phosphorus-nitrogen flame retardant technology achieves fire rating B1–B
Anti-mold and antibacterial MDF: Silver ions or organic anti-mold agents added, suitable for hospitals, food processing, etc.
Moisture-resistant MDF: Through paraffin emulsion optimization and MUF adhesive application, thickness swelling can be reduced to ≤6%
8.4 Digitalization and Intelligence
Online thickness detection, X-ray density curve monitoring, near-infrared moisture detection, and other digital quality control technologies are being introduced into MDF production lines, achieving full-batch quality traceability and real-time process adjustment, reducing random errors from manual sampling.
Medium Density Fiberboard (MDF) — Frequently Asked Questions (FAQ) Summary
Q1: What is Medium Density Fiberboard (MDF)? What is its essential characteristic?
A: Medium Density Fiberboard (MDF) is an engineered wood panel made from wood fibers or other plant fibers through fiber preparation, adhesive application, mat formation, and high-temperature hot pressing. Its density is typically between 650 and 800 kg/m³.
Unlike plywood (multiple veneers cross-bonded) and particleboard (particles bonded and pressed), MDF’s essential characteristic is that wood is reduced to a fibrous state and then reconstituted into a panel. This process eliminates natural wood knots, grain direction, and growth stresses, making MDF one of the most homogeneous and flattest engineered wood panels. It is especially suitable for surface finishing processes such as melamine facing, wood veneer facing, and paint coating.
Key data: High-quality MDF can achieve an internal bond strength of 0.6–1.2 MPa, a modulus of rupture of 25–40 MPa, and surface flatness deviation controlled within ±0.15 mm.
Q2: What are the characteristics of MDF’s raw material system and adhesive system?
A: MDF has a wide range of raw materials, including wood processing residues, fast-growing wood, and branches. Common raw material types include:
Poplar: Fine, long fibers with thin walls; light color and uniform texture. Used for high-end furniture and decorative panel substrates;
Pine: Longer fibers with higher resin content; good strength and yellowish color. Used for structural MDF and packaging;
Eucalyptus: Medium fibers with higher density; high strength. Used for load-bearing furniture and flooring substrates;
Mixed hardwoods: Balanced performance and lower cost. Used for general-purpose MDF;
Agricultural straw: Short fibers with high ash content; slightly lower performance, environmental concept. Used for low-cost eco-friendly panels.
JINDIWOOD technical standard: MDF products use 100% virgin poplar. Thin boards (≤9 mm) reach a density of ≥830 kg/m³; thick boards (>9 mm) reach ≥750 kg/m³.
Common adhesives include UF, MUF, MDI, and soy protein adhesive:
UF: Dosage 8–12%, E1/E0, ordinary indoor furniture;
MUF: Dosage 10–14%, E0/ENF, mid-to-high-end furniture, moisture-resistant boards;
MDI: Dosage 4–6%, ENF/HENF, formaldehyde-free boards, children’s furniture;
Soy protein adhesive: Dosage 10–15%, ENF grade, eco-friendly MDF.
MDF gluing is performed by atomized spraying and mixed with fibers in a high-speed mixer. The adhesive must have low viscosity and high penetration to uniformly coat each fiber.
Q3: What is the MDF production process?
A: The MDF production process mainly includes:
Chipping and screening: Logs or wood residues are processed into specified chips (length 15–30 mm, thickness 3–5 mm), removing oversized, undersized, sandy, and metallic impurities;
Fiber preparation — thermo-mechanical refining: Chips undergo pre-steaming (pressure 0.8–1.2 MPa, temperature 160–180°C, time 3–8 minutes) and refining. Disc gap: 0.1–0.5 mm;
Fiber drying: Wet fibers are dried by pipeline airflow with hot air at 160–200°C. Moisture content after drying: 8–12%; drying time: only 2–5 seconds;
Gluing: Dried fibers are metered and fed into a high-speed glue mixer. Adhesive is atomized and sprayed, with curing agent and paraffin emulsion added. Moisture content after gluing rises to 12–16%;
Mat forming: Air-laid or mechanical forming creates a fiber mat, followed by pre-pressing (0.5–1.0 MPa);
Hot pressing: Under high temperature and pressure, the adhesive cures, fibers densify, and the panel is stabilized;
Post-treatment: Cooling, conditioning for 48–72 hours, sanding, cutting, grading, and packaging.
Sanding usually involves three stages: coarse sanding (60–80 grit), medium sanding (100–120 grit), and fine sanding (150–180 grit). Sanding amount: 0.5–1.5 mm; surface roughness after sanding: Ra ≤3.2 μm.
Q4: Why is hot pressing the core of MDF production? What are the key parameters?
A: Hot pressing is the final stage that determines MDF density, strength, thickness precision, and environmental grade. Under high temperature and pressure, the mat undergoes adhesive curing, fiber densification, and panel stabilization. The hot-pressing cycle has three stages:
Stage 1: Compression — Pressure rises rapidly to 3.0–4.5 MPa, temperature 160–220°C; the mat is rapidly compressed, expelling air and moisture;
Stage 2: Curing — Pressure is maintained at 2.0–3.5 MPa; the adhesive crosslinks and cures, forming strong bonds between fibers;
Stage 3: Venting/Depressurization — Pressure gradually drops to 0, with natural cooling; internal steam pressure is released to prevent blistering.
Empirical formula for total hot-pressing time: Total time (seconds) ≈ board thickness (mm) × 8–15 s/mm. For 18 mm MDF, the cycle is about 150–270 seconds.
Key control points: thickness tolerance ±0.15 mm; temperature difference between mat surface and core should not be too large (≤20°C), otherwise “surface cured but core uncured” defects occur.
Q5: What are the core technical indicators of MDF?
A: According to GB/T 11718-2021, core MDF indicators include:
Density: 650–800 kg/m³; JINDIWOOD thin boards (≤9 mm) ≥830 kg/m³, thick boards (>9 mm) ≥750 kg/m³;
Internal bond strength (IB): Standard type ≥0.55 MPa, furniture type ≥0.65 MPa, load-bearing type ≥0.80 MPa;
Modulus of rupture (MOR): Standard type ≥23 MPa, load-bearing type ≥30 MPa;
Modulus of elasticity (MOE): Standard type ≥2700 MPa, load-bearing type ≥3500 MPa;
24-hour water absorption thickness swelling: Standard type ≤15%, moisture-resistant type ≤10%;
Formaldehyde emission: E1 ≤0.050 mg/m³, E0 ≤0.025 mg/m³, ENF ≤0.015 mg/m³;
Surface roughness: JINDIWOOD after sanding Ra ≤3.2 μm.
MDF’s modulus of rupture is lower than that of high-quality plywood, but its surface flatness and thickness uniformity are far superior, giving it an irreplaceable advantage in surface finishing applications.
Q6: What are the common classifications and grades of MDF?
A: MDF can be classified by density, use, and appearance.
By density:
Light MDF: <650 kg/m³, non-load-bearing decoration, model making;
Standard MDF: 650–800 kg/m³, furniture, decoration, decorative panel substrates;
High-density MDF (HDF): >800 kg/m³, flooring substrates, high-strength furniture.
By use:
Furniture type: IB ≥0.65 MPa, fine surface, for wardrobes, kitchen cabinets, tables and chairs;
Load-bearing type: MOR ≥30 MPa, higher density, for shelving, office desks, door panels;
Moisture-resistant type: thickness swelling ≤10%, for bathroom cabinets and kitchen furniture;
Flame-retardant type: fire rating B1–C, for public space decoration and hotels;
Low-formaldehyde type (ENF): formaldehyde emission ≤0.015 mg/m³, for children’s furniture and bedrooms.
By appearance: Premium grade, first grade, qualified grade. Common surface defects include black spots, white spots/glue spots, sanding marks, and carbonized spots.
Q7: What are the advantages and disadvantages of MDF compared with plywood?
A: MDF vs. plywood comparison:
Structure: MDF has uniformly distributed fibers and is nearly isotropic; plywood has cross-bonded veneers and more obvious anisotropy;
Surface flatness: MDF is excellent and suitable for fine finishing; plywood is good but shows veneer joint marks;
Edge treatment: MDF edges are dense and can be profiled; plywood edges show layered structure and require edge banding;
Screw holding: MDF is acceptable but loosens after repeated screwing; plywood is excellent, especially at edges;
Modulus of rupture: MDF is medium (25–40 MPa); plywood is high (50–100 MPa);
Moisture resistance: MDF is relatively poor; plywood is better;
Environmental performance: MDF uses more adhesive, making formaldehyde control more difficult; plywood uses relatively less adhesive;
Price: MDF is lower; plywood is higher;
Typical applications: MDF for decorative panel substrates, furniture components, and carving; plywood for load-bearing structures, construction formwork, and flooring substrates.
Q8: What are the common quality problems of MDF and their causes?
A: Common MDF quality problems include:
Thickness deviation and uneven density: Improper or worn thickness gauge on the hot press, uneven fiber distribution during forming, insufficient parallelism of hot-press platens. Solutions: regular calibration, optimized forming, hot-press maintenance;
Insufficient internal bond strength: Insufficient adhesive dosage, non-conforming adhesive quality, low hot-pressing temperature, excessively short fibers, insufficient curing agent. Solutions: optimize gluing, adjust hot-pressing parameters, test adhesive gel time;
Excessive thickness swelling: Insufficient or poorly dispersed paraffin, low density, insufficient hot-pressing cycle. Solutions: increase paraffin and optimize dispersion, moderately increase density, extend hot-pressing time;
Warping deformation: Excessive or uneven sanding, large moisture content difference between finished board and environment, insufficient conditioning, asymmetric density gradient. Solutions: control sanding amount, ensure sufficient conditioning, optimize forming;
Surface blistering: Too-fast venting at the end of hot pressing, excessive mat moisture content, improper hot-pressing temperature. Solutions: extend venting stage, reduce mat moisture content, optimize hot-pressing curve.
Q9: What are the technical development trends of MDF?
A: MDF technical development trends include:
Formaldehyde-free: MDI formaldehyde-free adhesives and bio-based adhesives are driving environmental grade improvements. HENF-grade MDF (formaldehyde emission ≤0.015 mg/m³) has entered mass production;
Lightweight and high-strength: Through fiber modification, foaming technology, or graded density structure, density can be ≤600 kg/m³ while maintaining sufficient mechanical strength, meeting lightweight needs for automotive interiors and aircraft cabins;
Functionalization: Flame-retardant MDF (B1–B), anti-mold and antibacterial MDF (silver ions or organic fungicides), moisture-resistant MDF (thickness swelling ≤6%);
Digitalization and intelligence: Online thickness measurement, X-ray density curve monitoring, near-infrared moisture detection, and other digital quality control technologies enable full-batch traceability and real-time process adjustment.
Q10: What are JINDIWOOD’s standards and commitments in the MDF field?
A: JINDIWOOD’s technical standards for MDF include: 100% virgin poplar raw material; thin boards (≤9 mm) density ≥830 kg/m³, thick boards (>9 mm) density ≥750 kg/m³; surface roughness after sanding Ra ≤3.2 μm; internal bond strength, modulus of rupture, and other indicators superior to conventional products.
JINDIWOOD’s commitment: From fiber to panel, every piece of MDF carries a promise of certainty, ensuring excellent processing performance, surface effect, and environmental controllability.
JINDIWOOD · Engineered for Certainty — From fiber to panel, every piece of MDF carries the promise of certainty.
This article is an original technical article by JINDIWOOD. Reproduction must indicate the source.